VPEG 2400 PCE Monomer for Concrete: Applications, Benefits & Selection Guide
Polycarboxylate ether (PCE) superplasticizers have become one of the most important technologies in modern concrete because their molecular structure can be tailored to provide high water reduction, improved flowability and controlled workability retention.
At the center of PCE synthesis is the polyether macromonomer.
VPEG 2400 PCE Monomer for Concrete is an unsaturated polyether macromonomer with an average molecular weight of approximately 2400 g/mol. It is designed as a raw material for synthesizing polycarboxylate superplasticizers rather than as an admixture that is added directly to concrete.
For PCE manufacturers, selecting a suitable macromonomer is important because monomer reactivity, molecular architecture, purity and batch consistency can influence polymerization behavior and, ultimately, the performance of the resulting superplasticizer.
This guide explains how VPEG 2400 works, where it is used, which specifications matter most, how it compares with other PCE macromonomers and what buyers should evaluate before placing a commercial order.
What Is VPEG 2400 PCE Monomer?
VPEG 2400 is a polyether macromonomer containing an unsaturated reactive group and a polyethylene oxide chain. During PCE production, the reactive group participates in free-radical copolymerization with acrylic acid and/or other functional monomers.
The resulting PCE generally has a comb-like molecular architecture consisting of:
- a polymer backbone containing adsorption or anchoring groups;
- polyether side chains extending into the aqueous phase;
- functional groups whose type and distribution can be adjusted during polymer design.
This molecular architecture is one of the main reasons PCE technology can provide much stronger dispersing performance than earlier generations of conventional concrete plasticizers.
Research on PCE systems has shown that the polymer adsorbs onto cement particle and hydration-product surfaces, while the polyether side chains generate steric repulsion that helps separate previously flocculated cement particles. This releases water trapped inside cement agglomerates and improves the flowability of the cementitious system.[1][2]
VPEG 2400 therefore should be viewed as a building block for PCE molecular design, rather than as a stand-alone concrete admixture.

Typical VPEG 2400 Product Parameters
For EverStar Group's current VPEG 2400 grade, representative specifications include:
| Parameter | Specification |
|---|---|
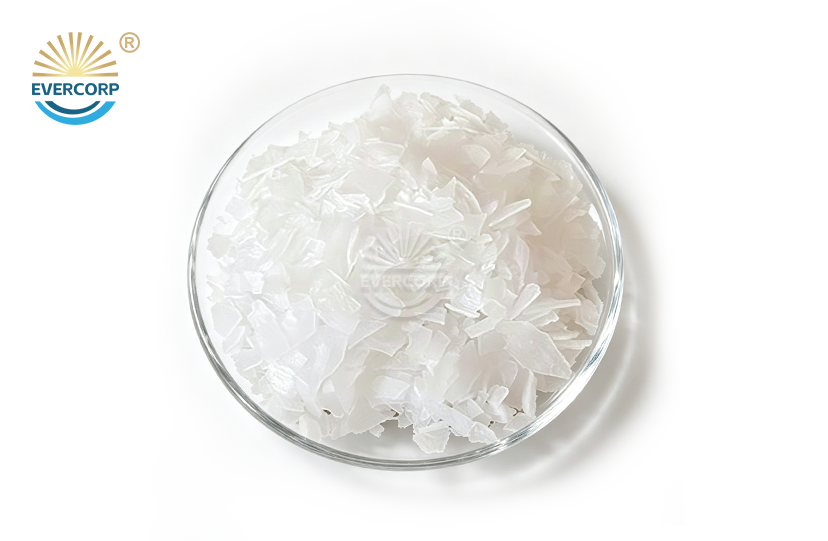
| Appearance | White or light yellow flakes |
| Average Molecular Weight | Approx. 2400 g/mol |
| Unsaturation | Approx. 0.3783 mol/kg |
| Hydroxyl Value | 22–25 mg KOH/g |
| Double Bond Retention | ≥92% |
| CAS Number | 31497-33-3 |
Product specifications may be adjusted as manufacturing processes and grades are optimized. Buyers should always confirm the latest TDS and batch-specific COA before commercial purchasing or formulation work.
Commercial naming conventions for PCE macromonomers can also vary among manufacturers and markets. For this reason, buyers should verify the chemical identity, technical specification and actual polymerization performance of a product instead of relying only on terms such as VPEG, HPEG or TPEG.
How Does VPEG 2400 Work in PCE Synthesis?

The concrete performance associated with VPEG does not come directly from the VPEG monomer itself. It develops after VPEG has been copolymerized into a properly designed polycarboxylate superplasticizer.
1. Formation of Polyether Side Chains
During polymerization, VPEG introduces long polyether side chains into the PCE molecule.
Once the finished PCE is added to cement paste, its adsorption groups can interact with cement surfaces while the hydrophilic polyether chains extend into the surrounding aqueous phase.
These side chains create steric hindrance between cement particles, helping prevent reflocculation.
The result can be improved dispersion and the possibility of producing concrete at lower water-to-binder ratios while maintaining the required workability.
2. Molecular Architecture Can Be Adjusted
PCE performance cannot be determined by molecular weight alone.
Side-chain length, grafting density, backbone composition, charge density, acid-to-ether ratio, molecular-weight distribution and functional comonomers can all influence adsorption, dispersion, rheology, setting behavior and slump retention.
Research by Winnefeld et al. demonstrated that changing the molecular architecture of comb-shaped PCE superplasticizers—including polyether side-chain length and density—significantly affects their behavior in cementitious systems.[3]
This is why two PCE products manufactured from macromonomers with similar nominal molecular weights may still perform differently in concrete.
3. High-Reactivity VPEG and Low-Temperature PCE Synthesis
One interesting development in modern PCE technology is the use of high-reactivity VPEG-type macromonomers.
A 2024 study published in Langmuir used a high-reactivity VPEG macromonomer to prepare different PCE structures under low-temperature reaction conditions. The researchers also demonstrated that changing the acid-to-ether ratio altered adsorption, cement fluidity and rheological behavior.[4]
This supports an important practical point for PCE manufacturers:
High-reactivity VPEG-type macromonomers can provide greater flexibility in designing efficient polymerization processes, including low-temperature synthesis under suitable initiator and formulation conditions.
However, reaction temperature, reaction time and conversion efficiency depend on the entire synthesis system. They should therefore be determined through laboratory and production trials rather than assumed from the monomer type alone.
Main Applications of VPEG 2400
The direct application of VPEG 2400 is the synthesis of polycarboxylate ether superplasticizers.
The resulting PCE formulations can then be designed for different concrete Applications.
1. High-Water-Reducing PCE Superplasticizers
VPEG-based PCE can be formulated for strong cement dispersion and efficient water reduction.
Such admixtures are commonly relevant to:
- high-strength concrete;
- high-performance concrete;
- pumping concrete;
- precast concrete;
- ready-mix concrete;
- self-compacting concrete;
- infrastructure concrete.
The actual water-reducing performance depends on the final PCE structure, dosage and concrete raw materials.
2. Slump-Retention PCE Systems
Ready-mix concrete may need to remain workable during batching, transport, pumping and placement.
PCE manufacturers can modify molecular architecture and formulation to control adsorption behavior over time and achieve the required balance between initial dispersion and workability retention.
VPEG 2400 can serve as one of the macromonomer building blocks in these formulations.
It is important, however, not to assume that a 2400 molecular weight automatically guarantees a specific slump-retention time. Cement composition, temperature, supplementary cementitious materials, aggregate quality and other admixtures can all affect final performance.
3. PCE for Variable Cement Chemistry
One of the most difficult challenges for admixture manufacturers is maintaining consistent performance when cement chemistry changes.
Sulphate is particularly important.
Research has shown that excessive sulphate ions in cementitious systems can competitively adsorb on cement surfaces and reduce the adsorption and dispersing efficiency of PCE superplasticizers.[5]
Alkali sulphates such as sodium sulphate and potassium sulphate can have particularly significant effects on PCE behavior.
For this reason, PCE manufacturers targeting markets with variable cement chemistry should evaluate VPEG-based formulations using actual local cement rather than depending only on a standard laboratory cement.
The correct question is therefore not:
“Is VPEG automatically sulphate-resistant?”
but rather:
“Can this VPEG grade help us design a PCE formulation that maintains satisfactory performance with the cement chemistry used in our target market?”
That question can only be answered through controlled compatibility testing.
4. High-Performance and Low Water-to-Binder Concrete
PCE technology is especially important in concrete systems where high flowability is required at a relatively low water-to-binder ratio.
Modern PCE superplasticizers have contributed to the development of high-performance concrete, self-compacting concrete and ultra-high-performance concrete by allowing cementitious materials to remain workable with reduced mixing water.[1][2]
VPEG 2400 can be used as a raw material in designing PCE systems for these applications.
Key Advantages of VPEG 2400 for PCE Manufacturers
1. Flexible Molecular Design
The biggest advantage of a modern polyether macromonomer is not a single fixed concrete performance number.
It is the ability to serve as part of a controllable molecular design platform.
By adjusting VPEG dosage, acid-to-ether ratio, chain-transfer system, initiator system and other comonomers, PCE manufacturers can develop formulations targeting different combinations of:
- initial dispersion;
- water reduction;
- workability retention;
- viscosity and flow behavior;
- cement compatibility;
- setting characteristics.
This flexibility is more valuable than claiming that one VPEG grade is universally better in every cement system.
2. High Reactivity for PCE Polymerization
Maintaining the reactive unsaturated functionality of a macromonomer is important for predictable copolymerization.
Parameters such as unsaturation and double-bond retention therefore deserve close attention during purchasing and incoming quality control.
Consistent reactive functionality helps manufacturers maintain more stable polymer architecture and batch-to-batch synthesis behavior.
3. Potential for Mild or Low-Temperature Synthesis
Research using high-reactivity VPEG has demonstrated successful low-temperature synthesis of PCE under specifically designed reaction conditions.[4]
For commercial manufacturers, this creates opportunities to investigate lower-temperature or shorter synthesis routes depending on:
- initiator chemistry;
- reactor configuration;
- monomer concentration;
- acid-to-ether ratio;
- chain-transfer agent;
- target PCE molecular weight.
Actual energy savings should be calculated from the manufacturer's own plant data instead of using a universal percentage.
4. Suitable for Different PCE Performance Targets
VPEG 2400 can be incorporated into PCE formulations designed for different market requirements.
However, the relationship between monomer structure and concrete performance is not linear. A longer side chain or higher molecular weight does not automatically mean better performance.
Scientific studies consistently show that the complete molecular architecture of PCE controls its interaction with cement.[2][3]
VPEG vs HPEG vs TPEG: What Should Buyers Know?

There is no simple rule stating that one macromonomer is superior to all others.
Different polyether macromonomers have different unsaturated structures and polymerization characteristics, while the final PCE performance is determined by both monomer chemistry and formulation design.
A practical comparison is:
| Factor | VPEG-Type Macromonomer | HPEG/TPEG-Type Macromonomers |
|---|---|---|
| Main Use | PCE synthesis | PCE synthesis |
| Polyether Side Chain | Yes | Yes |
| Unsaturated Reactive Group | Structure depends on grade | Structure depends on grade |
| Polymerization Behavior | High-reactivity grades are available | Mature commercial synthesis routes |
| Concrete Performance | Depends on final PCE architecture | Depends on final PCE architecture |
| Best Selection Method | Synthesis + cement compatibility testing | Synthesis + cement compatibility testing |
The international PCE market now includes several generations and structures of polyether macromonomers. Reviews of modern PCE technology describe HPEG and IPEG as major commercial systems while newer vinyl-ether PCE structures continue to broaden the available molecular design options.[2]
Therefore, procurement teams should avoid choosing a monomer only because it is described as a “new generation.”
What matters is whether the material produces the required PCE performance under your own synthesis and concrete conditions.
Key Specifications to Check Before Buying VPEG 2400
When evaluating VPEG 2400 suppliers, do not compare quotations by price alone.
Several technical parameters are more important for long-term production stability.
1. Molecular Weight and Distribution
A nominal molecular weight around 2400 indicates the approximate length of the polyether chain.
However, molecular-weight distribution is also important because broad variations may influence polymerization consistency.
Where necessary, manufacturers may use analytical methods such as GPC to evaluate molecular-weight distribution.
2. Unsaturation and Double-Bond Retention
The unsaturated group is responsible for incorporating the macromonomer into the polymer backbone during copolymerization.
Consistent unsaturation and good retention of reactive functionality therefore provide useful information about manufacturing control and storage stability.
Buyers should compare these parameters across multiple batches rather than relying on one sample.
3. Hydroxyl Value
Hydroxyl value is another useful quality-control parameter associated with the polyether structure.
For repeat purchases, consistency is generally more important than simply targeting an isolated number.
4. Moisture and Active Content
Moisture should remain within the supplier's specification.
Excessive variation in moisture changes the effective active-material content and may influence weighing accuracy, storage behavior, caking and formulation consistency.
5. Appearance and Handling
VPEG 2400 is commonly supplied in flake form.
Inspect incoming materials for unusual discoloration, excessive agglomeration, contamination or packaging damage.
Any significant difference from the approved sample or specification should be investigated before the material is released to production.
6. Batch-Specific COA
A reliable supplier should provide a Certificate of Analysis for commercial shipments.
The COA should correspond to the actual production batch rather than only showing a generic specification sheet.
For industrial PCE production, batch consistency is usually more valuable than an exceptionally good result from one laboratory sample.
How to Test VPEG 2400 Before Bulk Purchasing

A laboratory sample should be evaluated before changing a major PCE raw material supplier.
Step 1: Check Incoming Monomer Quality
Compare the sample against the supplier's specification and your existing approved raw material.
Relevant checks may include:
- appearance;
- molecular weight;
- unsaturation;
- hydroxyl value;
- moisture;
- double-bond retention;
- other parameters required by your internal QC system.
Step 2: Conduct PCE Synthesis Trials
Do not evaluate the macromonomer only as a raw material.
Use it in your actual or pilot-scale PCE synthesis process.
Keep major variables controlled so that the result can be compared with your existing monomer.
Record:
- reaction temperature;
- feeding time;
- reaction stability;
- conversion behavior;
- final solids;
- viscosity;
- pH;
- appearance;
- any unusual foaming or reaction behavior.
Step 3: Test With Local Cement
This is one of the most important stages.
Because PCE performance depends strongly on cement chemistry, test the synthesized PCE with the cement sources used in your target market.
Where possible, evaluate more than one cement.
Step 4: Evaluate Concrete Performance
Depending on the target application, testing may include:
- initial flow or slump;
- slump retention at different intervals;
- water-reduction performance;
- setting time;
- air content;
- rheology;
- compressive strength;
- compatibility with retarders, defoamers or air-entraining admixtures.
Only after both synthesis behavior and concrete performance are satisfactory should a commercial batch be approved.
Storage and Handling of VPEG 2400
VPEG 2400 should be stored according to the supplier's current SDS and technical recommendations.
General good practice includes:
- keeping the material in a cool, dry and ventilated warehouse;
- protecting packages from moisture;
- avoiding unnecessary exposure to high temperatures and direct sunlight;
- keeping unopened bags properly sealed;
- resealing partially used packages promptly;
- applying appropriate warehouse rotation practices.
Because storage conditions can influence the physical condition and quality consistency of polyether macromonomers, material that has been stored for an extended period should be inspected before use.
Always consult the latest SDS for personal protective equipment, spill response and handling requirements.
Quality Standards and Regulatory Documentation
It is important to distinguish between standards for the VPEG raw material and standards used to evaluate the finished concrete admixture.
ASTM C494/C494M specifies requirements for chemical admixtures added to hydraulic-cement concrete, including different classes of water-reducing, accelerating and retarding admixtures.[6]
Similarly, EN 934-2 defines requirements for admixtures used in concrete.[7]
These standards are highly relevant when evaluating the final PCE admixture, but they should not be described as product Certifications for the VPEG macromonomer itself.
When sourcing VPEG 2400 internationally, procurement teams should instead request the documentation relevant to the raw material and supplier, such as:
- Technical Data Sheet (TDS);
- Safety Data Sheet (SDS);
- batch-specific Certificate of Analysis (COA);
- quality-management certification;
- applicable REACH documentation for European supply;
- additional regulatory documentation required by the destination market.
How to Choose a Reliable VPEG 2400 Supplier
A reliable polyether monomer supplier should provide more than a competitive unit price.
Consistent Manufacturing
Ask how the supplier controls molecular weight, unsaturation, hydroxyl value and other key parameters.
Review several COAs where possible to understand batch-to-batch variation.
Technical Support
A supplier familiar with PCE production should be able to discuss polymerization behavior, quality parameters and compatibility-testing procedures.
Technical communication becomes especially important when changing monomer sources or developing a new PCE formulation.
Sample Availability
Laboratory testing before bulk purchasing reduces the risk associated with changing raw materials.
A supplier willing to provide samples, TDS, SDS and COA documentation makes technical evaluation easier.
Production Capacity and Supply Reliability
For large PCE manufacturers, supply continuity can be as important as price.
Discuss production capacity, lead time, packaging, loading quantity, shipping schedule and contingency plans before confirming a long-term supply arrangement.
Commercial Terms
Before ordering, confirm:
- MOQ;
- packaging;
- Incoterm;
- payment terms;
- production lead time;
- destination-port requirements;
- inspection requirements;
- batch documentation.
These details should be agreed before the first commercial shipment rather than after production has started.
FAQ
1. Is VPEG 2400 added directly to concrete?
No.
VPEG 2400 is a polyether macromonomer used to manufacture PCE superplasticizers. The finished PCE admixture, rather than the VPEG raw material itself, is normally dosed into concrete.
2. Why is the molecular weight approximately 2400?
A molecular weight around 2400 provides a commercially useful polyether chain length for designing comb-shaped PCE structures.
However, final concrete performance is controlled by the complete PCE molecular architecture—including side-chain density, backbone composition, charge density and molecular-weight distribution—not by the 2400 value alone.[3]
3. Does VPEG 2400 automatically provide better slump retention than HPEG or TPEG?
Not necessarily.
Slump retention depends on PCE molecular design, cement chemistry, dosage, temperature and concrete formulation.
VPEG can be used to develop high-performance formulations, but the correct comparison should be based on controlled synthesis and concrete testing.
4. Can VPEG-based PCE work with high-sulphate cement?
It may be possible to formulate PCE systems for cement with challenging sulphate chemistry, but compatibility should be tested.
Scientific research shows that excessive sulphate ions can compete with PCE for adsorption sites on cement surfaces and reduce dispersing efficiency.[5]
For this reason, buyers should test VPEG-based PCE with actual local cement rather than relying on a universal sulphate-resistance claim.
5. Can VPEG be used for low-temperature PCE synthesis?
High-reactivity VPEG macromonomers have been successfully used in published research to synthesize PCE under low-temperature conditions.[4]
Commercial reaction conditions still depend on the initiator system, comonomer ratio, reactor design and target polymer structure, so manufacturers should establish their own optimized synthesis process.
6. What documents should I request from a VPEG supplier?
At minimum, request:
- TDS;
- SDS;
- batch-specific COA;
- current product specification;
- applicable quality certificates;
- applicable REACH documentation for European markets.
A laboratory sample should also be tested before changing suppliers or placing a large commercial order.
Conclusion
VPEG 2400 is not simply another concrete chemical—it is a molecular building block used to design modern polycarboxylate superplasticizers.
Its value depends on how consistently it is manufactured and how effectively it performs during PCE polymerization.
For admixture manufacturers, the most important factors are therefore not unsupported claims about a fixed water-reduction percentage or universal slump-retention time. Instead, procurement and R&D teams should focus on:
- reactive functionality;
- molecular consistency;
- polymerization behavior;
- PCE molecular design;
- compatibility with local cement;
- batch-to-batch quality;
- technical documentation;
- supply reliability.
A well-controlled VPEG 2400 raw material, combined with a properly designed PCE formulation, can provide manufacturers with a flexible platform for developing high-performance concrete admixtures for ready-mix, precast, pumping and advanced concrete applications.
Partner With EverStar Group for VPEG 2400 Supply
EverStar Group supplies VPEG 2400 and other polyether macromonomers for polycarboxylate superplasticizer production.
For PCE manufacturers and construction-chemical companies, we provide:
- Factory-direct VPEG 2400 supply
- Production capacity: 150,000 MT/year
- MOQ: 1 FCL
- Samples available for laboratory evaluation
- TDS / SDS / COA available
- ISO and applicable REACH documentation
- Technical support for product evaluation
- Export supply for international markets
Before placing a commercial order, customers are encouraged to test the product using their own PCE synthesis process and local cement system.
For specifications and current commercial terms, visit our VPEG 2400 PCE Monomer product page or contact EverStar Group for a sample, technical documents and quotation.
Email: info@cneverstar.com
References
[1] Plank, J.; Sakai, E.; Miao, C. W.; Yu, C.; Hong, J. X. (2015). Chemical admixtures — Chemistry, applications and their impact on concrete microstructure and durability. Cement and Concrete Research, 78, 81–99. DOI: 10.1016/j.cemconres.2015.05.016.
[2] Lei, L.; Hirata, T.; Plank, J. (2022). 40 years of PCE superplasticizers — History, current state-of-the-art and an outlook. Cement and Concrete Research, 157, 106826. DOI: 10.1016/j.cemconres.2022.106826.
[3] Winnefeld, F.; Becker, S.; Pakusch, J.; Götz, T. (2007). Effects of the molecular architecture of comb-shaped superplasticizers on their performance in cementitious systems. Cement and Concrete Composites, 29(4), 251–262. DOI: 10.1016/j.cemconcomp.2006.12.006.
[4] Chang, Q.; Hu, M.; Liu, M.; Pang, J.; Liu, G.; Guo, J. (2024). Preparation of a Polycarboxylate Superplasticizer with Different Monomer Regulations and Its Effect on Fluidity, Rheology, and Strength of Cement. Langmuir, 40(11), 5673–5687. DOI: 10.1021/acs.langmuir.3c03021.
[5] He, Y.; Zhang, X.; Liu, S.; Hooton, R. D.; Ji, T.; Kong, Y. (2020). Impacts of sulphates on rheological property and hydration performance of cement paste in the function of polycarboxylate superplasticizer. Construction and Building Materials, 256, 119428. DOI: 10.1016/j.conbuildmat.2020.119428.
[6] ASTM International. ASTM C494/C494M — Standard Specification for Chemical Admixtures for Concrete.
[7] EN 934-2:2009+A1:2012. Admixtures for concrete, mortar and grout — Concrete admixtures — Definitions, requirements, conformity, marking and labelling.