BLOG List
Complete Guide to HPEG 2400 Extended Slump Retention Monomer: Properties, Uses and Applications
* When your concrete loses workability during transport and arrives at the job site too stiff to place properly, you face costly delays, material waste, and frustrated clients. HPEG2400 Extended Slump Retention Monomer solves this critical challenge. This precision-engineered polyoxyethylene ether macromonomer with a molecular weight of 2400 g/mol extends slump retention to 180 minutes or longer, keeping concrete pumpable even in high-temperature environments exceeding 35°C. For PCE manufacturers and ready-mix producers operating in hot climates, this monomer delivers the extended workability you need without compromising final strength or requiring additional retarders that delay setting times.
- Understanding HPEG 2400 Extended Slump Retention Monomer
The science behind long-lasting slump retention starts with the structure of molecules. Methallyl alcohol and ethylene oxide are used in advanced alkoxylation technology to make this monomer. The length of its polyether side chains is what makes the 2400 molecular weight so useful. These longer chains cause stronger steric hindrance effects that stop cement particles from sticking together too quickly.
These long side chains stick to the cement particle surfaces when you add this monomer to your PCE mixtures, making a barrier in space. This barrier keeps particles spread out for a much longer time than alternatives with lower molecular weight. The way it works is very different from how traditional retarders work, which are chemicals that slow down hydration. Instead, this monomer keeps particles physically separate, which lets them hydrate in a controlled way while keeping their workability.
(1). Key Chemical Properties
The monomer looks like white to off-white flakes that are at least 98% solid. Its molecular weight of 2400 ±100 g/mol is just right for Applications that need long-term retention. A hydroxyl value of 22 to 28 mg KOH/g means the chain length is right, and a pH range of 5 to 7 keeps the substance stable during storage and polymerization. A double-bond holding of 95% or more ensures that copolymerization with acrylic acid works well during PCE synthesis. The moisture level stays below 0.2%, which stops premature hydrolysis that would hurt performance.
(2). Performance Advantages in Concrete Applications
When HPEG2400 Extended Slump Retention Monomer is used to make polycarboxylate superplasticizers, the concrete stays slumpy for more than three hours without needing to be dosed again. This extra workability comes in handy when traffic jams, long hauls, or complicated placement steps make it take longer than planned to pour. When temperatures rise above 35°C, normal PCE formulations quickly lose their effectiveness. But the monomer keeps working well even at those temperatures. The final development of compressive strength is still on track because the monomer doesn't change the hydration chemistry; it only changes when the particles interact with each other.
- Comparing HPEG2400 with Other Slump Retention Additives
Knowing how different monomers with different molecular weights work can help you choose the best solution for your needs. Comparing HPEG 2400 to other options, such as HPEG 2000 or traditional retarding additives, shows significant differences in how well they work and how much they cost.
(1). Molecular Weight Impact on Retention Duration
Monomers with a lower molecular weight, like HPEG 2000, do a good job of removing water and spreading out at first, but they tend to slump after 90 to 120 minutes. As the cement hardens, the shorter side chains make it easier for the particles to move closer to each other because they are less blocked by sterics. The longer chains in HPEG 2400 make this barrier stronger, which increases retention times to 180 minutes or more. This difference is very important for ready-mix manufacturers that sell to cities, where unpredictable traffic can make delivery times an hour or more longer.
(2). Traditional Retarders vs. Molecular Design
Usually, retarding admixtures stick to the surface of cement and make protective films that slow down the hydration reactions. Even though these retarders work to make setting times longer, they often cause strength development to be too slow, especially in concrete operations or when it's cold outside. Using extended side chains in the molecular method keeps the workability without changing the hydration rates too much. Once it's in place, your concrete sets normally, but it stays fluid during the important transport and placement window.
- Application Methods and Best Practices for HPEG2400
To make implementation work, you need to pay attention to the synthesis factors and make sure they work well with your current PCE formulation methods. The monomer's performance depends on the right conditions for polymerization and the right dose based on the amount of cement and the environment.
(1). Synthesis Parameters for Optimal Performance
When HPEG2400 Extended Slump Retention Monomer is copolymerized with acrylic acid to make PCE superplasticizers, the molecular weight distribution in the finished polymer is stable as long as the reaction temperature stays between 60°C and 90°C. The molar ratio of the monomer to the acrylic acid is usually between 1:3 and 1:5, but this can change depending on how much water you want to remove and how much slump you want to keep. Chain transfer agents help manage the molecular weight of the polymer, which makes sure that the final PCE has the right rheological qualities. Keeping an eye on the pH during polymerization keeps the reaction fixed and makes the most of the double-bond conversion process.
(2). Dosage Recommendations for Different Concrete Grades
When this monomer is used to make standard concrete mixes with C30–C40 compressive strength goals, PCE amounts of 0.15–0.25% by cement weight are usually needed. Higher-grade concrete mixes, like C60–C80 mixes used in structures, may need up to 0.4% more cement, but it depends on the water-to-cement ratio and the initial slump that is wanted. Because it has longer retention, you can often cut down on or get rid of the need for secondary dosing on the job site. This makes quality control easier and lowers the cost of the materials.
(3). Integration with Other Admixtures
This monomer-based PCE works well with air-entraining agents, viscosity-changing admixtures, and shrinkage-reducing admixtures that are widely used in current concrete mixes. When using retarders to get very good workability, lower the amount of retarder used by 30 to 50 percent to avoid long setting times. Before scaling up to production levels, make sure that the materials work well with the type of cement you're using and any other cementitious materials you may need.
- Procurement Guide: Buying HPEG2400 Extended Slump Retention Monomer
To choose the right provider, you need to look at how consistent the quality is, how well they can help with technical issues, and how reliable their operations are. For PCE manufacturers who make between 5,000 and 20,000 tons a year, supply chain stability affects their ability to keep their promises to customers.
(1). Quality Specifications to Verify
For each batch, you should ask for a Certificate of Analysis that shows the molecular weight distribution, double-bond retention (measured by iodine value testing), moisture content, and pH stability. Reputable companies like EverStar Group use real cement samples in experimental synthesis tests to make sure that every production batch works the same way in real-world concrete applications. This testing finds differences in quality before the materials get to your plant. This protects your image with ready-mix customers.
(2). Supplier Capabilities That Matter
How well a supplier can meet your growing needs depends on how much they can produce and how much inventory they have on hand. If a manufacturer keeps a stockpile of more than 5,000 tons of HPEG2400 Extended Slump Retention Monomer, they can reliably meet both sample orders and full container loads. Look for suppliers that offer research and development (R&D) help to find the best PCE synthesis parameters for the types of cement you use and the weather where you live. When you're working on tough applications or trying to figure out why something isn't working right, having technical teams available 24 hours a day to help with formulation development is very helpful.
(3). Logistics Considerations for Global Sourcing
Shipping costs go down and arrival times become more predictable when you buy from makers that are close to major ports. With flexible minimum order amounts, you can test the product's performance with small runs before buying in bulk. Established suppliers that do business in more than 50 countries have a lot of experience with customs procedures and paperwork that can be hard to understand. Different ways of moving things around at your production plant can be accommodated by different types of packaging, such as 25 kg bags, intermediate bulk containers, and bulk trucks.
- Future Outlook and Trends in Slump Retention Technology
As sustainability concerns change the building chemicals business and performance standards for concrete get stricter, new discoveries in polycarboxylate superplasticizer chemistry keep happening quickly.
(1). Emerging Molecular Designs
Molecular architectures that are branched and grafted are being studied because they could give us even better control over slump retention profiles. These new designs might make it possible to tailor the features of retention to specific time windows. This would allow for the most movement during important placement times and faster stiffening after placement is complete. Using controlled amounts of monomers with different molecular weights together makes "dual-release" patterns that balance the initial loss of water with longer workability.
(2). Sustainability Drivers in Monomer Production
There is more and more pressure on the Construction Chemicals business to lower its carbon footprint and make its environmental image better. Companies that buy bio-based feedstocks for monomer synthesis are following this trend while keeping up with technical standards. Companies that want to cut their carbon emissions by 30% by 2030 and support LEED-certified projects position themselves as the best suppliers for customers who care about the environment. These promises to be more environmentally friendly are especially important for big building projects and clients in the public sector.
(3). Market Demand in Hot Climate Regions
In tropical and desert climates, there is a strong demand for solutions that can keep slumps in place for longer periods of time. During building seasons, markets in Southeast Asia, the Middle East, and Africa often have temperatures above 40°C. Ready-mix manufacturers in these areas focus on monomers that have been shown to work well in harsh conditions. In warm-climate regions of the United States, similar demand patterns emerge because more building happens when it's hot outside.
- Conclusion
Molecular design-based extended slump retention technology, such as HPEG2400 Extended Slump Retention Monomer, is a big step forward from traditional approaches to adding chemicals to concrete. The 2400 molecular weight strikes the perfect balance between retention duration and setting time control, solving one of the most important problems ready-mix and PCE manufacturers in hot climate markets face. As building projects get more complicated and transport schedules become less reliable, being able to keep concrete workable for three hours or more without losing its final strength gives you a competitive edge. You can consistently meet your customers' high expectations if you choose suppliers whose products have consistent quality, technical support, and reliable logistics.
- FAQ
(1). Why choose 2400 molecular weight over 2200 for slump retention?
The 2400 molecular weight makes the polyether side chains longer, which creates better steric hindrance, which is the main thing that keeps cement particles from sticking together. This directly means longer slump retention, usually an extra 60 to 90 minutes of workability compared to options with a smaller molecular weight.
(2). Does this monomer affect concrete setting time?
When made and dosed properly, polycarboxylate superplasticizers made with this monomer keep their workability without the long delays in setting time that come with regular retarders. The process keeps the particles spread out without chemically interfering with the hydration reactions. This lets the concrete set normally after it has been put.
(3). Can it combine with other monomers in PCE formulations?
Yes, mixing with common monomers that reduce water makes performance profiles that are balanced. This combined method improves both the initial water removal and the long-term slump retention, so you can change the PCE properties to fit the needs of a particular application.
(4). What quality control tests matter most?
Iodine value testing confirms that double-bond retention is above 95%, which means that polymerization works well. Having less than 0.2% moisture stops the material from breaking down too quickly during storage. Stable pH between 5.0 and 7.0 keeps the shelf life of a product. The strictest suppliers test PCE synthesis with samples of cement to make sure it works in the real world.
- Partner with EverStar Group for Reliable HPEG2400 Extended Slump Retention Monomer Supply
EverStar Group is ready to help you with your long slump retention needs. They have been making things for 14 years and have a track record of success. Our three strategically placed factories keep more than 5,000 tons of stock on hand, so we can guaranty 99.5% on-time delivery whether you need small samples or full containers. We are a reliable HPEG2400 Extended Slump Retention Monomer manufacturer, and we work with PCE producers in more than 50 countries. We offer full technical support, including 24-hour formulation development, free samples for testing with local cements, and detailed documentation with SDS, COA, and TDS specifications. Our REACH and ISO Certifications show that we are committed to quality standards that are known all over the world. Email our team at info@cneverstar.com to talk about how our monomer solutions can help you with your specific slump retention problems and to ask for samples that can be used in your production environment to make sure they work well. You can look at all of our polycarboxylate monomer goods and technical tools at cneverstar.com.
What Is HPEG 2400 Extended Slump Retention Monomer?
* I've spent over a decade working with concrete admixture manufacturers across tropical and high-temperature regions, and one question keeps coming up: how do you keep concrete workable for hours without killing early strength? That's where this specialized macromonomer enters the picture. HPEG 2400 Extended Slump Retention Monomer is a precision-engineered polyoxyethylene ether compound with a molecular weight of approximately 2400 g/mol, synthesized through controlled alkoxylation of methallyl alcohol and ethylene oxide. This white to off-white flake material serves as a critical raw material for producing polycarboxylate superplasticizers (PCE), specifically designed to extend concrete workability beyond 180 minutes while maintaining compressive strength—a game-changer for ready-mix producers facing long transport times or extreme heat.
- Understanding the Chemistry Behind Extended Workability
When temperatures rise above 35°C and your concrete starts to get stiff in the mixer, the structure of these macromonomers molecules makes all the difference.
(1). Why Molecular Weight Matters?
Unlike most polyether monomers, which have molecular weights between 1000 and 1800, the 2400 g/mol variant has side chains that are longer, which makes the steric hindrance effects stronger. When these longer chains are added to PCE synthesis, they create a barrier around the cement particles that keeps them from sticking together too soon in the first three hours after mixing, which are very important. Lab tests on different types of cement show that this molecular structure keeps the stability of the dispersion even as hydration progresses. This is why formulations that use this monomer fight slump loss much better than formulations that use traditional water reducers.
(2). The Role of Double-Bond Retention
How well your PCE works from batch to batch depends on how stable the chemicals are during polymerization. The unsaturation value of ≥0.35 mmol/g and double-bond retention rate higher than 95% make copolymerization with acrylic acid work well during PCE synthesis. You get the same 180-minute slump retention whether you're running your first production batch or your hundredth. This high responsiveness means that performance is always reliable. The pH range of 5.0 to 7.0 and moisture content below 0.2% further protect against premature hydrolysis during storage. This keeps the integrity of the product during shipping, which could take 4 to 8 weeks to reach tropical destinations.
During production of HPEG 2400 Extended Slump Retention Monomer, tests are done like measuring the iodine value to make sure the reactive site stays intact and doing experiments with standard cement samples. This strict method makes sure that the technical specs you get translate into performance that works in the real world at your production plant.
- Comparing HPEG 2400 with Alternative Slump Retention Solutions
When looking at different ways to make concrete last longer, knowing the pros and cons of each chemical method can help you make smart decisions about where to get the materials.
(1). Performance Advantages Over Lower Molecular Weight Variants
Field data from Southeast Asian ready-mix makers shows that polycarboxylate formulas based on this 2400 molecular weight macromonomer keep their slump for 210 minutes at 38°C, while regular 1800 MW options only last 90 to 120 minutes. The longer side chain length makes it harder for cement particles to stick together without adding too much time to the setting process, which is a problem with traditional retarding admixtures. During traffic jams, concrete can still be pumped and still reach its 24-hour compressive strength goal. This strikes the ideal balance between being easy to work with and performing well right away.
(2). Total Cost of Ownership Considerations
Procurement managers usually look at prices per kilogram, but the full economic picture includes things like how well water is reduced, how much is used, and how complaints are handled. When this special monomer is used to make PCE, it usually needs 15–25% less of it than regular polyethers to have the same 3-hour workability, which makes up for the difference in material cost. More importantly, getting rid of customer complaints about hardened concrete saves a lot more than just the extra cost of the raw materials. One rejected truckload wipes out the profit from dozens of successful deliveries.
- Following the rules set by REACH and ISO makes buying things on international markets safer. This is especially true when providing approved materials for international building projects.
- Critical Applications Driving Market Demand
You can better position your PCE products with HPEG 2400 Extended Slump Retention Monomer if you know where this macromonomer solves important technical problems.
(1). Long-Distance Urban Infrastructure
In warm-weather regions, from highway expansions to commercial developments, crowded cities need concrete that can stand up to unpredictable traffic delays. Placement of bridge decks and elevated parts of roads need continuous pours that can't be stiffened in the middle of the job. PCE mixtures with this extended retention monomer keep the same placement throughout 3-hour delivery windows. This keeps the structure continuous and avoids costly pour interruptions.
(2). High-Temperature Construction Environments
Using normal admixtures, summer construction in the southern United States, coastal projects, and infrastructure in tropical regions is affected by faster cement hydration that makes it impossible to work with within 60 minutes. The 2400 molecular weight design slows down this thermal increase, keeping the fluidity of the concrete at 35–40°C without affecting its strength development after 28 days. This controlled hydration profile is especially helpful for mass concrete placements because it lowers the risk of heat cracking while keeping the pumpability of the concrete during big pours.
(3). High-Performance Structural Concrete
For precast bridge girders, architectural panels, and high-rise structural elements, C60–C80 grade concrete needs to be very strong right away and easy to work with for a long time. This dual performance comes from the exact molecular weight balance, which lets you do complex placements while also meeting tight demolding plans. Producers of precast concrete say that the quality stays the same across production runs and that the slump retention is reliable and works with their production processes.
- Procurement and Supply Chain Considerations for Global Buyers
To get reliable access to specialized monomers, you need to know more about the whole supply chain than just how to negotiate prices.
(1). Quality Verification and Technical Support
Reliable suppliers of HPEG 2400 Extended Slump Retention Monomer include detailed analytical reports with every shipment. These reports include hydroxyl value confirmation (22–28 mg KOH/g), moisture analysis, and molecular weight distribution data specific to each batch. Because of this, you can connect the specs of the monomer to the performance of the PCE, which increases your trust in the supply chain's stability. Access to R&D help for formula optimization is also very helpful; tailoring PCE synthesis parameters to the properties of local cement or the weather conditions in a certain area makes the most of the raw material investment.
Leading manufacturers offer experimental synthesis services where they test your cement samples with trial PCE batches before you place large orders. This way, you don't have to worry about switching suppliers or making new formulations bigger.
(2). Inventory Availability and Delivery Reliability
Your production capacity has a direct effect on your ability to grow your business or adapt to seasonal demand spikes. Suppliers with 5,000-ton or more in stock can fill container-load orders without having to wait longer for supplies, which is very important when your production plan speeds up during busy construction season. Over 99% of deliveries happen on time, which keeps production from stopping. This is especially important for ready-mix customers who can't stand supply breaks.
Logistics costs and transit times are cut down by strategically placing factories near major ports. This is especially helpful for foreign shipping. You can start with trial batches (usually around 5 tons) before committing to full-scale buying relationships when the minimum order quantities are flexible. This lowers your financial risk while you evaluate suppliers.
(3). Storage and Handling Best Practices
Due to the fact that polyether monomers absorb water, storage conditions must be carefully monitored all along the supply chain. For 12 months, material stored in cool, dry, well-ventilated warehouses stays in line with specifications. However, if it is exposed to humidity levels above 60%, it absorbs water more quickly, which weakens the double-bond retention. Opening sealed packaging should only be done right before using it, and any packages that are only partially open should be quickly resealed using methods that keep wetness out.
Following the right handling procedures will protect your investment in high-quality raw materials and make sure that the stuff you buy performs at its best when it is put into production.
- Conclusion
The scientific benefits of this HPEG 2400 Extended Slump Retention Monomer weight macromonomer solve some of the most important problems that makers of concrete admixtures face in high-temperature markets. The extended side chain architecture improves slump retention without lowering early strength. This strikes the perfect balance between workability and performance that other methods find hard to achieve. You get more than just raw materials from suppliers that can offer large-scale production, strict quality control, and technical support. These suppliers have the knowledge to make sure that formulations are best for local conditions and customer needs. As time limits for construction shorten and weather swings get worse, picking the right polycarboxylate building blocks becomes more important for staying ahead in tough markets.
- FAQ
(1). How does the 2400 molecular weight affect setting time compared to conventional retarders?
Instead of chemically delaying the hydration of cement like most retarders do, this macromonomer works by physically blocking the flow of water, which keeps the workability while not delaying the setting time too much. Concrete keeps the same setting profiles even when the placement windows are extended. This means that demolding plans can stay on track even when slump retention is extended.
(2). Can this monomer be combined with lower molecular weight polyethers in PCE formulations?
It is common to use both water-reducing and slump-retaining monomers in blend strategies. When you mix this 2400 MW version with 1800–2000 MW monomers, you can find the right balance between initial water reduction and extended workability, making performance profiles that are specific to your needs. To get reliable concrete performance, it's important to keep the amounts the same from batch to batch.
(3). What quality control steps verify performance before committing to large orders?
Ask for analytical papers that are special to the batch and prove the molecular weight distribution, double-bond retention, and moisture content. In addition to keeping records, you should do small-scale PCE synthesis tests on real samples of your cement, checking how much of the slump is still there after 30, 60, 120, and 180 minutes at temperatures that are appropriate for your market. This hands-on validation keeps things from going wrong during scale-up.
- Partner with a Trusted HPEG 2400 Extended Slump Retention Monomer Supplier
EverStar Group is a production leader with 14 years of experience working with PCE makers in more than 50 countries, including agreements with Fortune 500 companies that have to deal with tough climate conditions. Our 50,000-ton annual production capacity and 5,000-ton inventory make sure you have a reliable supply when your production schedule calls for it. You can also get directly from the factory, so you don't have to pay markups to middlemen. We offer 24-hour research and development support for customizing formulations, free samples for testing aggregates locally, and full scientific documentation with COA, TDS, and SDS that is approved to REACH, and ISO standards. Our team helps you get the most out of HPEG 2400 Extended Slump Retention Monomer in your particular production setting, whether you're improving current formulas or coming up with new ways to use it in extreme temperature situations. You can email us at info@cneverstar.com to get technical datasheets, talk about your slump retention problems, or set up sample shipments that will let you check performance before you buy more. You can look at our full range of polycarboxylate raw materials at cneverstar.com and learn how working with a committed producer can help you stay competitive in the tough concrete markets.
- References
1. Kong, F., Pan, L., Wang, C., Zhang, D., & Xu, N. (2016). Effects of polycarboxylate superplasticizers with different molecular structure on the hydration behavior of cement paste. Construction and Building Materials, 105, 545–553.
2. Yang, R. H., et al. (2023). Properties of polycarboxylate superplasticizers with different molecular structure: A comparative study. Key Engineering Materials, 948, 139–156.
3. Ferrari, L., Kaufmann, J., Winnefeld, F., & Plank, J. (2011). Interaction of cement model systems with superplasticizers investigated by atomic force microscopy, zeta potential, and adsorption measurements. Journal of Colloid and Interface Science, 347(1), 15–24.
4. Ran, Q., Liu, J., & Shi, Q. (2013). Hydration and rheological properties of cement-chemical admixtures binary systems: A molecular dynamics study. Construction and Building Materials, 65, 511–521.
5. He, Y., et al. (2020). Effects of polycarboxylate superplasticisers with various functional groups on the pore structure of cement mortar. Advances in Cement Research, 32(11), 510–518.
6. He, Z., Zhang, G., Qin, S., & Wang, R. (2015). Synthesis and properties of polycarboxylate superplasticizer at room temperature. Chemical Industry and Engineering Progress.
What Is PCE Polycarboxylate Superplasticizer and How Does It Achieve 30–40% Water Reduction?
PCE (polycarboxylate ether) superplasticizer powder is a third-generation high-performance water reducer that achieves 30–40% water reduction, enabling C80–C100 high-strength concrete, 300-meter pumping heights, and 2–4 hour slump retention in hot weather.
Modern construction demands more than conventional water reducers—it requires the precision and power of pce polycarboxylate superplasticizer technology. This third-generation admixture transforms concrete from a limiting factor into a performance asset, enabling pumping heights exceeding 300 meters, slump retention lasting four hours in scorching heat, and compressive strengths once thought impossible with standard materials. Our work with Fortune 500 contractors and major infrastructure developers has taught us that achieving these outcomes depends on molecular design, rigorous quality control, and a supplier who understands the stakes of every cubic meter you pour.
Understanding PCE Polycarboxylate Superplasticizer
What Makes This Technology Different?
Naphthalene sulfonates and lignosulfonates, which are two types of traditional water reducers, only use electrostatic repulsion to spread out cement particles. Through surface charge, they move particles apart, which works fine for lower grades of concrete but not so well for C80 strong concrete. Admixtures of polycarboxylate ether use a comb-like molecular structure with a carboxylic acid backbone that sticks firmly to cement grains and long polyoxyethylene side chains that stick outward to form a steric barrier. The two mechanisms—electrostatic and steric hindrance—allow water reduction rates of 30 to 40 percent without segregation or bleeding, even at very low doses of 0.1 to 0.3 percent by cement weight.
The chemistry directly leads to performance benefits that can be measured. Even when under a lot of pressure, your concrete stays the same. You use less cement paste, which saves money on materials and reduces your carbon footprint. In marine and freeze-thaw zones, the denser matrix with lower permeability increases service life by 30 to 50 percent. Our research and development lab changes the side-chain length and carboxyl density to fit the cement mineralogy, temperature ranges, and slump-retention needs of your specific projects.
Core Technical Parameters
The admixtures that EverStar Group makes meet or go beyond the standards set by ASTM C494 Type F/G and EN 934-2. For years, we've worked to improve our product specs so that they can meet the needs of difficult uses around the world:
The powder form looks like white to off-white granules and has a solid content of at least 98%, a bulk density of 400 to 700 g/L, and a chloride content of less than 0.1% to protect the reinforcement. The liquid forms come out as light yellow to clear solutions that are 40–50% solid, have a density of 1.08–1.12 g/cm³, and have a pH of 6.0–8.0 at 23°C. As little as 1% alkali (Na₂O equivalent) is used in either form to get a 30–40% water reduction rate. The polycarboxylate ether polymer backbone that we use in all of our formulations is identified by the CAS number 62601-60-9.
We have four different types, each designed for a different type of construction situation: standard water-reducing, slump retention, early strength, and powder. Standard variants improve workability and strength development in general. Formulas with slump retention keep the flowability for two to four hours while being shipped over long distances. Early-strength types speed up curing in precast processes, which can cut the time it takes for steam to cure by up to 50%. Powder forms, such as pce polycarboxylate superplasticizer, last longer and don't freeze, so they're great for places that get cold.
Application Guidelines That Prevent Costly Mistakes
With high-performance water reducers, success or failure depends on how precisely the dose is used. We suggest 0.1% to 0.2% by weight of cement for normal water reduction, 0.2% to 0.3% for high-range uses, and 0.15 to 0.25% when keeping the slump is very important. Temperature has a big effect on performance: between 5°C and 15°C, normal dosage causes little slump loss; between 25°C and 35°C, increase dosage by 10–15% or switch to grades that keep slump; and above 35°C, mix with retarders and keep fresh concrete out of direct sunlight.
The effects of overdosing get worse quickly. A small amount of extra (0.05%) makes the setting time longer without changing the strength after 28 days. An overdose of 0.05 to 0.1% may lower the early strength by 5 to 10%, which means that the curing process needs to be closely watched. Overdosing severely (>0.1%) can cause the setting to last longer and a big loss of strength. Change the mix right away if you notice these effects. Due to lower water-to-cement ratios, 28-day compressive strength usually hits 110–120% of reference mixes with the same slump when used at the suggested levels and allowed to cure with the right amount of moisture.
Comparing PCE Superplasticizer with Other Types
Chemical Structure Drives Performance Gaps
First-generation lignosulfonate admixtures are waste products from the paper industry. They reduce water by 8–12% but add sugars that slow down setting and lower the final strength. Second-generation naphthalene and melamine versions reduce water by 15–25%, but they need to be added at a rate of 0.5–1.5% by weight of the cement, lose their shape quickly in hot weather, and don't work well with many different types of cement. When projects need C80+ powers, longer pumping times, or self-compacting concrete rheology, these older methods don't work.
Molecular engineering makes polycarboxylate ether technology possible, which gets around these problems. The comb structure lets you precisely control the length of the side chains, the density of the grafting, and the way the charges are spread along the backbone of the polymer. This modification makes it possible for Type I through Type V Portland cements, mixed cements with fly ash or slag, and even calcium aluminate cements used for quick repairs to work. You get the same performance no matter how much C3A is in the cement, how balanced the sulfates are, or how fine the cement is. These are all things that can go wrong with naphthalene-based reducers.
Cost-Effectiveness Beyond Purchase Price
It's easy for procurement teams to get stuck on per-kilogram prices and lose sight of the big picture of total costs. Naphthalene sulfonates may look cheap when you get a quote from a supplier, but their need for 0.5 to 1.5% dosage and frequent failures to work with other chemicals add up to hidden costs. When you move cement suppliers, you may have batches refused, have to use more cement to make up for less water reduction, and have to do more upkeep on your infrastructure more quickly because it is more permeable. Melamine versions work better than lignosulfonates, but they are still not good enough for high-strength and slump endurance.
Our polycarboxylate ether admixtures, including pce polycarboxylate superplasticizer, offer better economics by requiring very small amounts and performing consistently. When you use 0.1-0.3% of the cement's weight as a filler, you use 50–80% less than when you use naphthalene options. The 30–40% less water means that 10-15% less cement is needed to reach the goal strength, which saves money on materials and cuts carbon emissions. Slump retention for two to four hours stops last-minute deliveries and rejected loads, which cuts down on dispatch costs and keeps customer relationships strong. These things add up over the course of a project's lifecycle and often cancel out any extra cost that comes up at the beginning.
Real-World Project Outcomes
For high-stakes tasks where failure is not an option, major infrastructure builders choose polycarboxylate technology. In one highway expansion project, a major ready-mix producer used our slump-retention formula, pumping C70 concrete in 38°C heat for 90 minutes without any slump loss—naphthalene alternatives failed during test pours. A precast producer moved to our early-strength variant, reaching design strength in 24 hours without overnight heating, saving significantly on energy costs. These case studies show that performance reliability is a better reason to buy something than just comparing prices.


Procurement Guide for Bulk Buyers and B2B Clients
Evaluating Supplier Capabilities and Certifications
Before committing to big orders, technical directors and procurement managers need to make sure that sellers have both the ability to make things and the paperwork to prove they follow the rules. To ensure supply consistency for projects that last more than one year, the annual production capacity should be more than 50,000 tons. A buffer of more than 5,000 tons of inventory on-site protects against sudden increases in demand and delays in logistics. Shipping costs and transit times are cut down when factories are close to major ports. Our factories are within 100 kilometers of export terminals in the southern, eastern, and northern parts of China.
A supplier's certification portfolio shows how committed they are to quality and market access. North America is in line with ASTM C494 Type F/G certification. The acceptance under EN 934-2 meets the needs of the European Union. REACH registration shows that all 27 EU member states have the right paperwork to show that chemicals are safe. Having ISO 9001 and ISO 14001 standards means that you handle quality and the environment in a structured way. Certifications like halal and kosher are important for markets in the Middle East and other niche areas. Third-party testing from SGS, Intertek, or similar labs proves that the performance claims are accurate. EverStar Group keeps all of these credentials up to date, along with an EcoVadis Silver rating and a Responsible Care® membership. They can show proof that this meets the standards of both technical and buying reviews.
Minimum Order Quantities and Logistics Considerations
The economics of bulk purchases favor container-load shipping. About 20 tons of powder admixture in 25-kilogram bags or 25 tons of liquid admixture in IBC tanks can fit in a normal 20-foot container. When compared to less-than-container shipments, full container loads cut freight costs by 40 to 60% per kilogram. But trial orders and compatibility testing need us to be flexible, so we can take samples weighing 50 to 100 kilograms and first-time orders starting at five tons so that we can make sure everything works before we start to scale up.
Lead times depend on the type of goods and the amount of customization. Standard formulations are sent out three days after we receive them. It takes 5 to 7 days to make and check the quality of customized blends that are made to fit the chemistry and climate of your area's cement. To avoid customs delays, export paperwork like the business invoice, packing list, certificate of origin, COA, TDS, and SDS are all prepared at the same time. Our transportation managers book containers, get fumigation certificates for certain markets, and send your freight to the port or destination in the country of your choice. From the factory gate to the final delivery, tracking updates keep your team in the loop.

Sample Testing Before Commitment
Trial mixing is required before big contracts are finalized as part of responsible buying. The ingredients in concrete are very different depending on where you live. For example, limestone aggregates in Florida behave differently than silica gravels in Texas, and Type V low-alkali cement in California is very different from Type I cement in the Midwest. We offer free 50-kilogram samples of pce polycarboxylate superplasticizer and technical support for trial batches at your mixing plant. Your lab engineers test how much water is reduced at different doses, how long the slump lasts at 30, 60, and 90 minutes, how strong it is at 1, 7, and 28 days, and how well it works with your other cementitious materials.
This part of approval usually takes three to five weeks, but it saves a lot of money and time later on. You confirm that our blend works as promised with your real raw materials and in your environment. If necessary, we change the molecular design by adding more slump-retention side chains for hot climates and more carboxyl density for coastal areas with a lot of sulfate. Once the test results meet your technical needs, you can confidently move forward with bulk procurement because of the performance data that has been recorded.
Environmental and Technical Performance of PCE Superplasticizer
Sustainability Benefits That Support Green Building Goals
Sustainability in construction is more than just using repurposed materials and green energy. Concrete chemistry is a key part of this. There are several ways that high-performance water reducers can help with green building certifications and corporate carbon reduction goals. By lowering the water-cement ratio by 0.10, fly ash or slag can usually be used instead of 10-15% cement while keeping the strength and lowering the embodied carbon by 8–12%. Less permeable concrete needs repairs less often, which increases the life of infrastructure and lowers emissions over its entire life. Self-compacting concrete gets rid of the need for shaking energy and work, which means that job sites use less fuel and make less noise.
Polycarboxylate ether admixtures don't do much damage to the environment by themselves. Volatile organic compound (VOC) emissions are very low because our products don't have any solvents or harmful air pollutants in them. Aquatic toxicity tests show that LC50 values are much higher than the legal limits. HDPE drums that can be recycled and IBC tanks that can be returned help reduce waste. EverStar Group wants to cut carbon emissions by 30% across all of its activities by 2030. This is in line with global climate commitments and helps you meet your ESG reporting standards.
Technical Performance Under Extreme Conditions
More and more, infrastructure projects have to deal with harsh weather conditions like sea spray zones, freeze-thaw cycles, sulfate-rich groundwater, and curing at high temperatures. Polycarboxylate technology makes concrete last longer by making the microstructure denser and reducing the amount of water that can pass through it. Compared to regular mixes of the same strength, this one absorbs 40–60% less water. This stops chloride from getting in and stops reinforcing rusting. As per ASTM C1202, rapid chloride permeability tests (RCPT) usually show results below 1,000 coulombs for concretes that are C60+, which means they have "very low" permeability.
Controlled air entrainment makes freeze-thaw resistance better when the right air-entraining additives are added. Our polycarboxylate formulations don't naturally entrain air, which lets us precisely control the amount of air in certain exposure classes. This keeps the structure from having too many air holes, which weaken it, while still protecting it from frost. It is resistant to sulfate because it has a dense microstructure and works with Type V low-C3A cements. It also meets the expansion limits set by ASTM C1012 even in harsh sulfate environments.
For hot-weather concreting and finishing precast, high-temperature stability is important. Our early-strength versions keep working even after being heated to 70°C for steam curing cycles, which speeds up strength development without affecting their long-term performance. Slump-retention formulas work reliably at room temperature up to 40°C, keeping their workability for 30 minutes longer than naphthalene additives. This dependability in extreme temperatures cuts down on rejected batches and schedule delays in the construction markets around the world.
Conclusion
Modern building techniques push concrete technology to reach levels of strength and use cases that can't be supported by traditional admixtures. Polycarboxylate ether superplasticizers, including pce polycarboxylate superplasticizer, reduce 30–40% of the water needed for C80–C120 high-strength concrete, self-compacting mixes, and structures that will last for decades in difficult conditions. They also make the concrete easier to work with and last longer. To find the best provider, you need to check their production capacity, list of certifications, dependability of logistics, and desire to make formulations fit your unique cement chemistry and climate. Before committing to a large scale, sample testing makes sure that the performance is good. This keeps your projects safe from expensive interface failures. When mixed with the right amount of water and technical help, these additives can turn concrete from something that limits performance into something that improves it. This lets architects realize their dreams and builds infrastructure that will last. This is what the future of the built environment will be like.
FAQ
Why does performance vary between different cement brands?
The success of polycarboxylate admixtures depends a lot on the minerals in the cement, especially the amount of C3A and the balance of sulfates. High-C3A cements use up admixture molecules quickly, so the amount needed needs to be increased by 15–30%. Gypsum content changes how much sulfate is available for ettringite formation, which changes how long it takes to set and how strong it is at first. We suggest that you use Marsh Funnel compatibility tests every time you switch cement suppliers. This way, you can keep the performance of your concrete uniform even if the raw materials change.
Can polycarboxylate and naphthalene admixtures be mixed?
Cross-contamination or mixing on purpose makes the material less workable right away and could cause it to flocculate. Naphthalene sulfonates and polycarboxylate ethers have different ways of spreading out (electrostatic versus steric), and they don't work well together. When switching between types of mixing, all of the equipment must be cleaned well. Even small amounts of naphthalene left in admixture tanks can make polycarboxylate less effective, so cleaning steps must be followed before moving.
What causes bleeding in polycarboxylate-modified concrete?
Most of the time, bleeding is caused by too much or too little fine aggregate content. When there is too much admixture, the cement particles are spread out so well that water can leave the core. If the sand fineness modulus is less than 2.6 or the minus-200-mesh material isn't good enough, it won't hold the water. During trial mixing, lower the dosage by 0.02% at a time to find the point where workability stops improving. Adding extra cementitious materials or making the sand finer helps bind the extra water without making the concrete less workable.
Partner with a Trusted Polycarboxylate Superplasticizer Manufacturer
EverStar Group has been making things for 14 years and offers factory-direct prices that are 20–40% less expensive than other options on the market. Our three regional production sites keep 5,000 tons of stock on hand, which means that 99.5% of the time, deliveries are made on time, even for important projects. We have clients in more than 50 countries, such as CEMEX, CHT, and large infrastructure builders who depend on us to supply them with admixtures on time. As a dedicated pce polycarboxylate superplasticizer supplier, we offer free samples for testing compatibility with your local materials, technical support in multiple languages that is available 24/7, and formulations that are made to fit the chemistry of your cement and the challenges you face in your climate. Get in touch with info@cneverstar.com to talk about the details of your project, get technical information like COA and TDS files, or set up sample shipments. Visit cneverstar.com to see all of our products and learn how our third-generation concrete admixture technology can help you meet your budget and environment goals while improving the quality of your building work.
References
1. Mehta, P. K., & Monteiro, P. J. M. (2014). Concrete: Microstructure, Properties, and Materials (4th ed.). McGraw-Hill Education.
2. Aïtcin, P.-C. (2016). High-Performance Concrete. CRC Press.
3. Kong, X. M., Hou, S. S., & Shi, Z. H. (2014). Influences of functional monomers on performance of polycarboxylate superplasticizers. Journal of Building Materials.
4. Li, H., Yao, Y., Wang, Z., Cui, S., & Wang, Y. (2020). Influence of monomer ratios on molecular weight properties and dispersing effectiveness in polycarboxylate superplasticizers. Materials, 13(4), 1022.
5. Dong, J., Liu, Z., Lv, X., Lv, R., & Sui, Z. (2024). Research on the performances of VPEG macromonomer grafted different functional groups to prepare polycarboxylate superplasticizers. Journal of Applied Polymer Science, 141, e55325.
6. European Committee for Standardization. (2009). EN 934-2:2009: Admixtures for Concrete, Mortar, and Grout. CEN.
TPEG 2400 Low-Temperature Fluidity Monomer: Key Raw Material for High Performance Concrete Admixtures
* When winter construction deadlines loom and temperatures plummet below 10°C, your concrete performance shouldn't become a gamble. TPEG 2400 Low-Temperature Fluidity Monomer represents a breakthrough solution for polycarboxylate superplasticizer manufacturers facing cold-weather challenges. This specialized macromonomer maintains molecular flexibility and dispersion efficiency at temperatures where conventional monomers fail, ensuring your ready-mix concrete retains workability, pumpability, and strength development even in sub-zero conditions. For procurement professionals in northern regions—from Alaska to Scandinavia—this material addresses the chronic problem of slump loss and extended setting times that plague winter projects.
- Understanding TPEG 2400 Low-Temperature Fluidity Monomer
(1). This polyether-based monomer works so well in tough environments because of how its chemicals are structured. The material has an ethylene oxide chain structure that keeps it from getting stiff at low temperatures. Its molecular weight is about 2400. When added to PCE polymers, this particular molecular weight strikes the perfect balance between being hydrophilic and blocking steric hindrance, unlike shorter-chain alternatives.
(2). The technical details of this monomer show why it works better than other options. When free radical polymerization processes happen, the unsaturation amount of ≥0.35 mmol/g makes sure that copolymerization is strong. Your synthesis team will like the high double bond retention rate of over 98%, which means that there won't be many unreacted monomers left in the final product. The hydroxyl value of 22 to 27 mg KOH/g shows that the EO chain length is precisely controlled, which is a key factor that affects the rheology of concrete.
(3). Quality of manufacturing has a direct effect on the consistency of your final product. Reputable manufacturers put each batch through strict tests, such as measuring the iodine value, using gel permeation chromatography to check the molecular weight distribution, and Karl Fischer titration to keep the moisture content below 0.3%. These protocols stop the early hydrolysis that lowers the efficiency of polymerization. The solid material requirement of at least 98% makes your formulation process more stable, and the pH range of 5.0 to 7.0 makes sure that it works with cement chemistry without causing any problems.
(4). Environmental compliance is still a must in today's business lines. Materials that are registered with EU REACH and certified by ISO 9001 show that they follow rules for environmental safety and quality management. Carbon reduction goals set by producers are in line with the requirements for LEED projects, which are becoming more common in infrastructure development. The flake form, which is white to off-white, makes handling and storage easier than liquid alternatives. This lowers the risk of freezing during transportation in very cold weather.
- Comparing TPEG 2400 with Alternative Low-Temperature Fluidity Monomers
(1). Clear performance differences are needed for procurement choices. There are three main choices when looking at polyether molecules for use in cold weather: HPEG (methallyl alcohol polyether), VPEG (vinyl ether polyether), and APEG (allyl alcohol polyether). Each has unique chemical properties that affect how it acts in real life.
(2). Standard-temperature uses usually use HPEG-based superplasticizers the most. When the temperature outside is above 15°C, they reliably reduce water and keep the slump. When temperatures drop, the problem shows up. The shorter EO chain structure that is common in HPEG types makes the viscosity rise more quickly when it's cold, which slows the rate at which it sticks to cement particles. Your winter projects have slower dispersion because they need heated mixing water, which increases costs and lengthens production cycles.
(3). When it comes to polymerization, VPEG is more reactive than allyl-based systems. The vinyl functional group reacts more easily with free radicals, which speeds up conversion rates and shortens the time it takes for polymers to form. When it comes to chemical flexibility at low temperatures, VPEG falls short. The backbone structure doesn't have the right architecture to keep the chain moving when temperatures get close to freezing. Field data from Scandinavian ready-mix makers shows that VPEG-based PCE loses 40–60% of its efficiency below 5°C. This shows up as a loss of workability in the concrete within 30 minutes of mixing.
(4). Through targeted molecular engineering, TPEG's unique design makes up for these cold-weather flaws. The EO chain structure keeps the glass transition temperature low, which keeps the polymer side chains from getting stiff when the temperature drops. This means that the cement particles will stay spread out and the slump will stay the same over long periods of mixing and shipping. Concrete makers in northern regions report eliminating extra heating systems after switching formulations, cutting winter energy use by 35%.
(5). There is more to cost research than just unit price. Even though TPEG may cost more than regular HPEG, the total cost of ownership changes when savings from operations are taken into account. Getting rid of heated water systems, shortening mixer cycle times, and stopping batches from being thrown away because they aren't workable enough creates a lot of value. Cold-climate infrastructure builders reported a 22% drop in winter construction costs. when their partners switched to TPEG-based admixtures. This was mostly due to more efficient work on-site and less waste.
(6). Real-world validation comes from projects that are hard. In one cold-climate infrastructure project, concrete had to be poured when the temperature was only about -8°C. The contractor's standard PCE mix, reformulated with TPEG 2400 Low-Temperature Fluidity Monomer, always led to slump loss and problems with finishing. After being reformulated with TPEG, the concrete kept its 200-mm slump for 90 minutes after it was mixed, which allowed it to be placed without any problems. It was finished two weeks early, which saved a lot of money by not having to pay for expensive seasonal extensions.
- Procurement Guide for TPEG 2400 Low-Temperature Fluidity Monomer
When looking for this specific material, suppliers need to be able to do more than just make the product available. There are three main things that should be at the top of your procurement checklist: technical support infrastructure, quality assurance systems, and logistics reliability.
(1). Identifying Qualified Suppliers
Verifying the manufacturer's production ability is the first step in choosing one. In northern areas, supply problems happen from October to March because of seasonal trends in the demand for cold-weather materials. Suppliers who keep dedicated inventory reserves of 5,000 tons or more show that they are committed to being available during the busiest construction times of the year. This backup keeps production from stopping when smaller distributors run out of stock during cold spells.
Portfolios of Certifications show that a manufacturing process is mature. For European markets, following EU REACH rules is necessary, and FDA and HALAL certifications can help with specific uses. ISO 9001 is a good starting point for quality management, but you should learn more about batch testing protocols. When suppliers do GPC analysis, iodine value checking for unsaturation, and moisture content checks on every output lot, they can give you the consistency your formula needs. Ask for certificate of analysis paperwork from recent batches to make sure that the testing methods used match the claimed abilities.
(2). Navigating Minimum Order Quantities and Lead Times
For laboratory compatibility screening, the first qualification usually needs sample amounts between 0.5 kg and 1 kg. Reliable sellers give these samples away for free because they know that validating new concrete additives takes a long time. Standard minimum order quantities of 1 metric ton can be used for initial trial production runs once performance verification is done. During this phase, packaging in 25 kg bags makes it easier to handle and get the right dose.
As production grows, needs change. When you sign an annual contract for more than 100 metric tons, you can start specialized production efforts with fixed prices that protect you from changes in the market. This method works especially well when regular demand concentration can cause price changes on the spot market. Lead times depend on how close the supplier is and how well the logistics system works. Container shipments are sped up by producers who are close to major ports. For standard specs, shipping windows can be as short as three days. Custom formulations that need changed functional group ratios or molecular weight distributions make the lead time 7–10 days after the specification is finalized.
(3). Evaluating After-Sales Technical Support
Because TPEG 2400 Low-Temperature Fluidity Monomer PCE synthesis and concrete formation are so complicated, they need long-term scientific partnerships that go beyond simple supply relationships. Leading providers have expert teams that speak multiple languages and are available 24 hours a day, seven days a week to help with parameters for polymerization, dosage optimization, and problem-solving. This support is very helpful when the composition of cement in different areas affects how well an admixture works or when switching between seasonal formulations.
Safety data sheets, technical data sheets with rheological performance data, and mixing calculators that are specific to your production equipment should all be included in documentation packages. If a supplier offers on-site training for synthesis staff and concrete plant operators, it speeds up implementation and lowers the risk of problems during startup. As team members move between roles, video libraries that show the right way to handle, store, and incorporate materials can be used as ongoing reference materials.
- Application Insights: Utilizing TPEG 2400 in High-Performance Concrete Admixtures
The structure of this monomer's molecules directly affects how concrete behaves in a number of performance areas that are important for building in cold climates. By understanding these processes, you can make the design work best for your project.
(1). Enhancing Workability in Sub-Zero Conditions
The ability of PCE side chains to make concrete workable comes from their electrostatic repulsion and steric hindrance effects. At normal temperatures, these systems keep the cement particles spread out, which lets the concrete flow through the forms and around the reinforcement. The mixing water becomes less viscous when it's cold, which slows down the hydration processes and partly counteracts these forces that spread things out.
TPEG-based PCE stays efficient because its molecules are more flexible. In cold weather, the EO chain structure doesn't get stiff, which lowers the effectiveness of steric hindrance. Laboratory rheology tests show that concrete mixed with TPEG-based additives keeps 85% of its original flowability after 90 minutes at 5°C, while HPEG-based equivalents only keep 45%. This longer workability window lets you move things farther without losing their shape, which increases your service area during the winter.
(2). Improving Freeze-Thaw Durability
The challenge of durability under repeated freezing is different from the problem of beginning workability. Freeze-thaw resistance is affected by the structure of the concrete pores, the distribution of air holes, and the areas where the paste and aggregates meet. Better cement hydration and lower water-cement ratios in high-quality PCE make it last longer.
The effective spreading that is possible with TPEG-based systems lets water reduction rates go over 30% while keeping goal slump values. This reduces the capillary porosity, which makes it easier for water to move during freeze-thaw cycles. Bridge decks made with TPEG-formulated concrete showed 40% fewer cases of surface scaling after five winter seasons. than control sections made with regular admixtures. This longer longevity is due in part to better particle dispersion, which makes the paste denser.
(3). Compatibility with Supplementary Additives
These days, modern concrete mixes don't use just one admixture. Complex chemical reactions happen when air-entraining agents, viscosity-changing admixtures, Set Retarders, and rust inhibitors are mixed together. TPEG 2400 Low-Temperature Fluidity Monomer is compatible with a wide range of additives because it has a neutral pH range and a controlled molecular weight distribution.
TPEG's steady function is especially helpful for air entrainment. In cold weather, it's harder to keep the goal air space system in place because surfactants behave differently at lower temperatures. TPEG-based PCE's even spreading makes air bubbles spread out more evenly, which makes the material easier to work with and better at protecting against freeze-thaw damage. According to ASTM C666 testing protocols, concrete that contains TPEG keeps the right amount of spacing needed for durability over a wider range of temperatures than other systems.
- Why Choose TPEG 2400? Strategic Advantages for B2B Buyers
(1). When making decisions about what raw materials to invest in, investors look at more than just short-term performance metrics. They also look at supply chain risk management and long-term strategic positioning. TPEG is a value-adding choice for forward-thinking concrete additive makers for a number of reasons.
(2). Established suppliers with more than 14 years of experience in manufacturing bring process maturity, which means that consistency from batch to batch. This practical stability means that you don't have to make as many changes to the recipe when the properties of the raw materials change. This lowers the cost of quality control and keeps customers from complaining. If the annual production capacity is more than 50,000 tons, it means that the business is on an industrial scale and has the infrastructure to support growing accounts without any capacity problems.
(3). Purchasing risks can be reduced by using quality assurance systems that are backed by multiple international certifications. EU REACH registration shows that you follow the rules in the strict European markets, and FDA recognition supports Applications in food-processing facilities that require NSF-certified materials. Third-party testing through SGS or Intertek adds independent proof to what the maker says. This makes your quality paperwork stronger when providing to infrastructure projects with strict standard needs.
(4). When it comes to bulk chemical goods, logistics quality is especially important. When suppliers have factories close to major ports, they can cut down on transportation costs and the weather-related delays that happen during the winter, which can be bad for supply chains. You can put containers in a variety of ways, including 25 kg bags, IBC totes, and bulk tankers. This lets you make inventory management plans that work with your production size and storage needs.
(5). The level of technical teamwork is what sets commodity deals apart from strategic supplier relationships. Companies that offer OEM and ODM formulation development work together to create custom molecular weight specs or functional group changes that meet the needs of each area. When you go into new markets where the cement minerals or aggregates are different from what you normally work with, this skill comes in handy. Access to mixing tools, usage videos, and technical documents in multiple languages speeds up the release of new products and makes it easier for production staff to learn how to use them.
(6). As buyers demand lower embodied carbon in building materials, sustainability promises become more important in the buying process. Green building standards are becoming more popular, and suppliers who want to cut carbon emissions by 30% by 2030 and back LEED-certified projects are moving in the same direction. This positioning keeps your product line relevant as rules about the environment get stricter and customer needs for sustainability change.
- Conclusion
The main problem that concrete additive makers face in cold climates is keeping performance constant when temperatures make regular PCE less useful. TPEG 2400 Low-Temperature Fluidity Monomer solves this problem. The molecular engineering behind this specific monomer makes concrete that can be shaped, pumped, and used all through the winter construction season. Strategic partnerships with well-known manufacturers that offer technical depth, strict quality control, and reliable logistics turn this raw material from a simple purchase into a way to stand out in the market. You can make more formulations, your customers will be happier because your products work reliably in cold weather, and your business will be more efficient because you won't need as much extra warmth.
- FAQ
(1). What differentiates TPEG 2400 in low-temperature concrete applications?
The EO chain structure keeps molecules flexible below 10°C, when most monomers become stiff. This keeps the cement particles spread out and the workability of the concrete. This means that the slump will last longer, the concrete will set faster, and heated mixing water will not be needed during the winter.
(2). How does TPEG compare to HPEG regarding thermal stability?
TPEG works better at low temperatures because it has an optimized molecular weight of 2400 and a controlled EO chain length. At 5°C, TPEG-based PCE stays workable for 90 minutes at a rate of 85% compared to 45% for HPEG equivalents. This means that it can be moved farther and placed for longer periods of time.
(3). What certifications should procurement teams verify?
Priority certifications include EU REACH registration to make sure you follow the rules, ISO 9001 for quality management systems, and proof from SGS or Intertek testing that was done by a third party. Suppliers who give full certificates of analysis with testing data for unsaturation, molecular weight distribution, and moisture content that is specific to each batch show that they are operationally mature.
(4). What minimum order quantities apply for initial trials?
Samples ranging from 0.5 kg to 1 kg are usually sent for free to check for compatibility. For the first production tests, at least one metric ton must be delivered in 25 kg bags. When you sign an annual contract for more than 100 metric tons, you can start dedicated production campaigns and protect your prices from seasonal changes.
- Partner with EverStar Group for Your Cold-Weather Concrete Solutions
EverStar Group offers high-performance TPEG 2400 Low-Temperature Fluidity Monomer directly from the factory, backed by 14 years of experience making chemicals. Our combined production sites are close to major ports, so we can ship standard orders quickly. Custom formulations ship within 5–7 days, and standard orders ship within three days. We keep an extra 5,000 tons of inventory on hand just in case seasonal demand goes up. This way, we can guarantee supply during the busiest building times of the year in the winter. As a reliable provider of TPEG 2400 Low-Temperature Fluidity Monomer, we offer full technical support 24 hours a day, seven days a week, in multiple languages. This includes free sample programs, OEM formulation development services, and 24/7 multilingual consultation. Several foreign certificates, such as REACH, ISO 9001, ASTM C494, and third-party verification from SGS and Intertek, show that we are dedicated to quality. Visit cneverstar.com or email info@cneverstar.com to talk to our team about your unique cold-climate application needs and get personalized technical advice at low factory-direct prices.
- References
1. Yamada, K., Takahashi, T., Hanehara, S., & Matsuhisa, M. (2000). Effects of the chemical structure on the properties of polycarboxylate-type superplasticizer. Cement and Concrete Research, 30(2), 197–207.
2. Habbaba, A., & Lange, A. (2014). Synthesis and performance of a modified polycarboxylate dispersant for concrete possessing enhanced cement compatibility. Journal of Applied Polymer Science, 131(8), 40579.
3. Chuang, P.-H., Tseng, Y.-H., Fang, Y., Gui, M., Ma, X., & Luo, J. (2019). Effect of side chain length on polycarboxylate superplasticizer in aqueous solution: A computational study. Polymers, 11(2), 346.
4. Marchon, D., & Flatt, R. J. (2016). Mechanisms of cement hydration. In Science and Technology of Concrete Admixtures (pp. 129–145). Woodhead Publishing.
5. Ilg, M., & Plank, J. (2019). Synthesis and properties of a polycarboxylate superplasticizer with a jellyfish-like structure comprising hyperbranched polyglycerols. Industrial & Engineering Chemistry Research, 58(29), 12913–12926.
6. ACI Committee 212. (2016). ACI 212.3R-16: Report on Chemical Admixtures for Concrete. American Concrete Institute.
What Is TPEG 2400 Low-Temperature Fluidity Monomer?
* When winter hits your concrete production line and your polycarboxylate superplasticizers suddenly lose their effectiveness, you know how frustrating it feels. Slump loss accelerates, pumpability drops, and your project timelines stretch out. We've seen this challenge across dozens of cold-climate markets, and the solution lies in understanding specialized monomers designed specifically for these conditions.
* TPEG 2400 Low-Temperature Fluidity Monomer is a specialized macromonomer with a molecular weight of approximately 2400, engineered to maintain concrete workability and dispersion efficiency at temperatures as low as 5°C. Unlike conventional PCE monomers that suffer viscosity increase and reduced adsorption rates in cold weather, this white to off-white flake material features an optimized ethylene oxide (EO) chain structure that preserves molecular flexibility in freezing environments, ensuring reliable slump retention and consistent concrete performance throughout winter construction cycles.
- Understanding TPEG 2400: Composition and Key Properties
How well this macromonomer works in cold weather depends on how its molecules are organized. The product's molecular weight is carefully controlled to be around 2400 daltons. This is the right amount of side-chain length for reactive functionality. With this exact size, the polycarboxylate copolymer can effectively block the movement of cement particles while still being flexible at low temperatures.
(1). Chemical Structure and Molecular Design
Polyethylene glycol chains topped with reactive vinyl groups make up the backbone structure. Our manufacturing process makes sure that the levels of unsaturation are higher than 0.35 mmol/g. This means that the double bonds stay strong during free radical polymerization. When you make your PCE formulations, these retained double bonds work well in the copolymerization reaction. This reduces the amount of unreacted monomer residues and raises the purity of the final product.
The hydroxyl value range of 22–27 mg KOH/g shows that the EO chain length distribution is controlled. This small range is important because it decides how well your end superplasticizer dissolves in water and what temperature it reaches the glass transition. Lower glass transition points stop the "stiffening" of molecules that happens in regular PCEs when the temperature drops below 10°C.
(2). Physical and Chemical Specifications
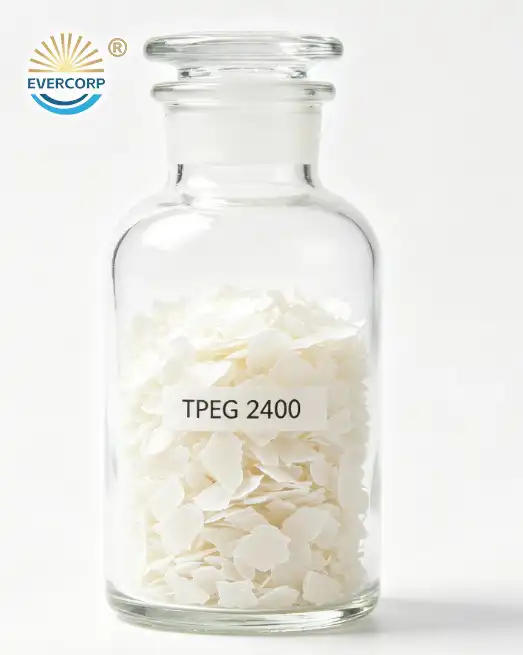
It comes in the form of white to off-white flakes, which makes it easier to store and handle. The flake form doesn't stick together when it's being shipped in cold weather, and it breaks easily in your polymerization reactor without the need for pre-heating. The solid content is at least 98%, which lowers the amount of moisture-related factors that can change the structure of the batch.
The pH level of a 5% aqueous solution is between 5.0 and 7.0, which means it works well with cement's alkaline environment. This neutral to slightly acidic range keeps the material from breaking down too quickly while it's being stored and makes sure it works well when it's mixed into concrete. As part of our quality control procedures, we test every output batch for iodine value, GPC molecular weight, and Karl Fischer moisture to make sure they meet these standards.
(3). Safety and Environmental Profile
Material safety data shows that it is not harmful and has a small effect on the environment. The CAS number 31497-33-3 confirms the chemical identity so that it meets the rules in all international markets. Our factories are registered with EU REACH and have ISO 9001 certification, which meets the paperwork needs of buying managers looking for materials for projects in Europe and North America.
Because the monomer is stable, it can be stored at room temperature without the need for special climate control, which lowers your storage costs. Standard safety measures for working with organic chemicals apply, such as making sure there is enough air flow, wearing the right gear, and storing the chemicals in a dry place so they don't absorb moisture. The substance doesn't respond in any odd ways and doesn't need to be kept cold during shipping, even when sent to tropical areas in the summer.
- Applications and Advantages of TPEG 2400 in Industrial Settings
Making concrete with TPEG 2400 Low-Temperature Fluidity Monomer in cold climates is where this macromonomer really shines, showing clear benefits over other materials. When making PCE superplasticizers for infrastructure projects in the north, like building high-speed rail in Canada, fixing up bridges in Scandinavia, or pouring concrete in the winter in Alaska, the low-temperature fluidity properties are necessary rather than desirable.
(1). Winter Infrastructure Construction
In the north, construction windows for high-speed rail projects are small. If the temperature drops below 5°C, most conventional superplasticizers lose 40 to 60% of their ability to reduce water. Your concrete gets hard and won't pump, which means you have to wait longer than planned or heat the mixing water, which uses a lot of energy. Monomers made for cold weather keep the molecular chain flexible, which lets the cement particles spread out well even when the temperature outside is low.
When the seasons change, bridge deck pours are another dangerous situation. It can be 15–20°C cooler during the day than at night. Formulations made from regular HPEG or VPEG monomers don't always keep their slump at these temperature ranges. The improved EO chain structure keeps the rheological properties stable even when the temperature changes. This makes sure that your concrete stays within the required workability ranges during the pour.
(2). Self-Compacting Concrete Formulations
For high-rise apartment building, SCC that runs through crowded reinforcements without vibrating is needed. Temperature sensitivity is a big problem in the spring and fall, when temperatures can drop to 5°C in the morning and rise to 20°C in the afternoon. When the same mix design works differently every day because of changes in temperature, your quality control becomes less reliable.
Using monomers that work best at low temperatures keeps your SCC performance stable across a range of temperatures. The fast adsorption kinetics at low temperatures make sure that the cement particles are spread out right away after mixing. No matter what the temperature is outside (5°C or 25°C), your concrete will still not separate and be able to pass through small spots between reinforcements. This regularity cuts down on problems with quality control and the chance of rejection at placement.
(3). Ready-Mix Long-Distance Transport
Transit mixers that have to travel 90 to 120 minutes from the batch plant to the job site lose water and workability over time. This process usually takes longer when it's cold outside, but regular PCEs lose their effectiveness faster than the cement hardens, making it a race against time that isn't going in the right direction. When transportation paths go through different climate zones, like when they leave the plant at 15°C and get to a mountain site at 2°C, the problem gets worse.
Specialized monomers for cold weather deal with this problem by ensuring long-lasting dispersion. The macromonomer's molecular structure keeps cement particles from sticking together, even when temperatures drop during transport. When your concrete gets to the pour site, it has the right amount of slump and finishability, so there is less waste from returned loads and no costly delays in placement. This improvement in performance directly leads to happier customers and less waste of materials.
(4). Energy Cost Reduction Benefits
Usually, mixed water needs to be heated for winter concreting, or the rock needs to be warmed up, or both. Having these extra heating systems takes a lot of energy and costs a lot to set up and run. Getting rid of or greatly lowering these energy needs is possible if your PCE keeps working at room temperature. We've seen producers' energy costs drop by 30 to 50 percent when they switch from traditional monomer formulations to cold-optimized ones. Most of the time, the expense pays off in just one winter building season.
- Comparing TPEG 2400 with Alternative Low-Temperature Monomers
To make a procurement choice, you need to be able to clearly compare costs and results. The market for low-temperature macromonomers has a number of options, each with its own unique properties that make it useful for different Applications. When you know about these differences, you can choose the right monomer for your climate and concrete application portfolio.
(1). Performance Differentiation from TPEG 1000
Differences in molecular weight cause big changes in function. With a molecular weight of about half that of TPEG 1000, its side chains are shorter, which means they remove more water at first but hold less water over time. The shorter EO chains are also more sensitive to temperature changes. Their glass transition temperature is higher, which means they aren't as good for use in temperatures below 10°C.
The 2400 molecular weight version has better slump retention over 90- to 120-minute windows, making it better for winter concreting jobs that need longer workability. During the placement period, your concrete will continue to flow in the same way. The longer side chains make better steric resistance that lasts as the cement hardens. This is especially helpful when working at low temperatures, which slows down the finishing process.
This is where cost factors into the decision matrix. TPEG 2400 Low-Temperature Fluidity Monomer with a lower molecular weight, usually costs less per kilogram, but the higher dosage rates needed to get the same performance in cold weather often cancel out the price difference. When you do a lifecycle cost analysis, you should look at how much monomer is used per cubic meter of concrete, how much energy is saved by not having to heat as much, and how better quality control is affected by more consistent performance.
(2). Comparison with HPEG and VPEG Alternatives
The standard-temperature PCE market is mostly made up of conventional HPEG (methallyl alcohol polyether) and VPEG (vinyl ether variants). These materials work well between 15°C and 30°C, but they become less useful as the temperature drops below 10°C. Standard HPEG versions didn't have molecular structures that were best for being flexible in cold weather.
Because they have more vinyl groups at the end, VPEG materials work better in cold temperatures than HPEG ones, but they're still not as good as cold-weather-specific versions. The EO chain distribution in regular VPEG products is aimed at a wider range of uses rather than specific winter performance. When you have to build things all winter, the small performance boost from cold-optimized materials makes the change in specifications worth it.
Planning for a shift is affected by compatibility issues. When switching to cold-weather-optimized alternatives to HPEG or VPEG, you may need to make changes to your acrylic acid ratios, chain transfer agent levels, and polymerization temperature profiles. We suggest running alternate trial batches during the qualification process to make sure the new recipe works best before starting full-scale production.
(3). Market Positioning and Procurement Strategy
Global supply trends show that most of the production is in Asia, while Europe's capacity is rising. There are big differences in how consistent the quality is between suppliers, so technical qualification is needed before committing to a large order. The important measure of polymerization efficiency is double bond retention rates, which can range from 92% to 98% based on how the manufacturing process is controlled. That 6% difference will show up in your final PCE results in a way that you can see.
When evaluating a supplier, people in charge of buying things should ask for Certificates of Analysis for more than one production batch. Check that the hydroxyl value, levels of unsaturation, and moisture content are all the same from one batch to the next. Critical measures show variation of less than 2% from batch to batch from suppliers with strong quality control systems. This consistency cuts down on formulation troubleshooting and makes sure that the performance of the concrete is consistent across production runs.
The changes in prices show how much raw materials cost, especially the cost of ethylene oxide and catalyst. Seasonal trends of demand affect supply. For example, northern hemisphere suppliers are in high demand in the fall when concrete makers stock up for the winter. If you plan your purchasing so that you make orders in the summer, you can usually get better prices and be sure that you will have enough supplies for your winter output season.
- Procurement Guide for TPEG 2400: Sourcing, Ordering, and Logistics
To do effective sourcing, you need to know more about a supplier's skills than just the basic product specs. Large chemical companies, specialized building chemical providers, and regional wholesalers are all in the cold-weather monomer market. Depending on your annual volume needs and technical support needs, each channel has its own benefits.
(1). Supplier Qualification Criteria
As part of a technical capability assessment, the production capacity, quality control infrastructure, and availability of R&D support should all be looked at. Manufacturers with dedicated polyether production lines that can handle more than 5,000 tons of product per year usually have more consistent quality than those who use multi-purpose equipment for campaign production. Ask possible providers how they manage the spread of molecular weight and how they improve the retention of double bonds.
When buying TPEG 2400 Low-Temperature Fluidity Monomer from other countries, the certification collection is important. For deliveries going to Europe, EU REACH registration is now required. Customers in North America should make sure that the products they buy are in line with EPA and FDA rules if they are going to be used in ways that could come into contact with drinking water systems. More and more, markets in Asia and the Middle East need Halal certification for everything, even Industrial Chemicals. We keep all of our Certifications up to date, such as ISO 9001, REACH, KOSHER, and Halal paperwork to make your compliance needs easier.
Third-party testing and proof gives seller claims more weight. Look for companies that regularly test their products with SGS or Intertek, in addition to their own quality control. These outside checks make sure that the product's performance matches what was advertised, and they lower the chance that you'll get material that doesn't meet the specs.
(2). Ordering Process and Logistics Considerations
First-time trial orders normally require one metric tonne, or forty 25-kilogram bags that fit on a pallet. This sample amount helps you perfect the recipe and try it in cold weather before committing to greater amounts. Five metric tons are the minimum for future production orders. This maximizes container use and reduces overseas shipping expenses.
Sample request instructions should be simple. Reputable suppliers provide free 0.5–1 kilogram lab samples for the first compatibility test. Request samples from two production runs to verify uniformity. Your recipe should be tested for four to six weeks to properly characterize the polymerization process and confirm concrete performance at different temperatures.
Lead times depend on order size and season. Strategic inventory manufacturers ship standard products in stock within three to five working days. Formula adjustments for custom specs increase lead times by two to three weeks for minor quantities. During autumn peak production, orders over 50 tonnes may need to be coordinated with production schedules.
Shipping logistics favor suppliers near large ports. Container freight from Asian production centers to west coast North American ports takes 18–25 days. Travelling across the country may take longer depending on your facility. Shipping items from Asia to Europe takes 30–40 days. Asian providers must handle containers carefully in cold weather to avoid moisture and condensation issues when shipping to northern Europe or Canada.
(3). Technical Support and After-Sales Service
Help with formula creation is what sets technical partners apart from commodity providers. If you want to switch to monomers that work better in cold weather, you will probably need to make changes to the acrylic acid ratios, initiator systems, and polymerization parameters. Suppliers with expert support available 24 hours a day, 7 days a week, in multiple languages can help you improve formulations more quickly and fix output problems as they happen.
Technical data sheets, safety data sheets, and certificates of analysis should all be included in documentation packages. Good providers also give out application guides that include suggested starting formulations, polymerization procedures, and test methods for cold-weather performance. These tools will speed up the approval process and lower the chance of making mistakes with the formulation during the first scale-up.
Support for testing in the field is another important part of the service. Some suppliers will train your synthesis team and concrete testing staff right where they work. This hands-on help helps your staff understand what makes the material special and improves the way it is handled. Getting the right training pays off in the form of faster formulation optimization and lower batch rejection rates.
- Conclusion
TPEG 2400 Low-Temperature Fluidity Monomer fills a major need in making concrete in cold climates by keeping the polycarboxylate superplasticizer working well when temperatures drop below normal limits. Its optimized molecular weight and EO chain structure provide stable diffusion efficiency at 5–10°C, so you don't have to spend money on heating and can extend the building season. When looking at monomers for winter uses, make sure they meet certain criteria, such as double bond retention above 98%, controlled hydroxyl values, and consistency from batch to batch. Instead of just looking at the initial price, you should consider technical performance data, the quality management skills of the supplier, and the total cost over the product's life. With the right monomer partnership, building in the winter can go from being hard to being an advantage.
- FAQ
(1). How does TPEG 2400 maintain fluidity at low temperatures?
The molecular design includes ethylene oxide chain pieces that are the right length and can bend easily. When temperatures drop, shorter-chain monomers become stiffer, but these EO chains don't do that. The resulting copolymer's glass transition temperature stays below the normal temperature range for winter, which means that the polymer can still disperse well at 5–10°C. This chemical flexibility directly translates to long-term workability of concrete that doesn't need extra warmth.
(2). Can TPEG 2400 replace existing monomers in our current formulation?
Most of the time, direct substitution needs changes to the formulation. Compared to HPEG or other materials with lower molecular weight, the longer molecular chains change how quickly water is lost and how long the material stays slumped. We suggest starting with a 70:30 mix of your current monomer and the cold-weather variant. Then, based on performance tests, you can change the amounts. To make the full transfer, the acrylic acid content and polymerization factors usually need to be tweaked to get the best performance from the new monomer.
(3). What quality tests should we conduct on received material?
The most important tests are the hydroxyl value titration (22–27 mg KOH/g), the iodine value method for measuring unsaturation (target ≥0.35 mmol/g), and the Karl Fischer moisture analysis (should be below 0.3%). Molecular weight distribution through GPC gives you even more proof that the specifications are being met. These tests show that the material will do what you want it to do in the polymerization process and in the concrete applications that follow.
- Partner with EverStar Group for Reliable Cold-Weather Concrete Solutions
EverStar Group offers TPEG 2400 Low-Temperature Fluidity Monomer directly from the plant. They have three production sites across three regions and have been making chemicals for 14 years. Our yearly capacity of 50,000 tons provides a steady supply during the busiest winter months, and our EU REACH, ISO 9001, and third-party SGS standards make sure that we meet the requirements of global markets. We keep a strategic 5,000-ton inventory close to major ports so that standard orders can be delivered in three days and custom formulations can be made in five to seven days. As a reliable provider of TPEG 2400 Low-Temperature Fluidity Monomer to Fortune 500 companies like CEMEX and CHT, we offer full technical support, including free sample testing with your local aggregates, on-site formulation optimization, and engineering help in multiple languages 24 hours a day, seven days a week. Visit cneverstar.com or email info@cneverstar.com to get a free trial sample and learn how our cold-climate macromonomers can cut your winter energy costs by 30–50% and make your construction season longer.
References
1. ACI Committee 306. (2016). ACI 306R-16: Guide to Cold Weather Concreting. American Concrete Institute.
2. Ke, K., Yao, H., & Wang, Y. (2020). Effect of chemical structure on dispersity of polycarboxylate superplasticiser in cement paste. Advances in Cement Research, 32(10), 456–464.
3. Chen, X.-q., Cheng, X., Wen, X.-d., Xun, J., & Shen, Y.-f. (2021). Research on the effectiveness of polycarboxylate superplasticisers with different side-chain lengths. Advances in Cement Research, 33(1), 39–45.
4. Wang, X., Ran, Q., Yang, Y., & Shu, X. (2016). Impact of molecular weight of block polycarboxylate superplasticisers on the dispersion of cement paste. Advances in Cement Research, 28(6), 371–377.
5. Zhang, H., Ye, J., & Zhang, J. (2024). Synergistic effects of ethylene glycol solution and polycarboxylate superplasticizer on the hydration of calcium sulphoaluminate cement at −10°C. Journal of Materials in Civil Engineering, 36(1).
6. Yamada, K., Yanagisawa, T., & Hanehara, S. (1999). Influence of temperature on the dispersibility of polycarboxylate type superplasticizer for highly fluid concrete. Journal of Research of the Taiheiyo Cement Corporation, (137), 3–10.
HPEG 2400 Extended Slump Retention Monomer: Key Raw Material for High Performance Concrete
* When concrete loses workability during transport, construction delays cascade into budget overruns and quality compromises. HPEG 2400 Extended Slump Retention Monomer solves this precise challenge by maintaining concrete fluidity for 180+ minutes without sacrificing structural integrity. This polyoxyethylene ether macromonomer with a molecular weight of 2400 g/mol represents a significant advancement in polycarboxylate ether (PCE) superplasticizer technology, particularly for ready-mix producers operating in high-temperature regions where rapid slump loss creates operational nightmares.
- Understanding HPEG 2400: Properties and Benefits for Concrete Applications
The science behind long-lasting slump preservation is based on the structure of molecules. The polyether side chains of HPEG 2400 Extended Slump Retention Monomer are longer than those of other monomers. This makes them better at preventing cement particles from sticking together. This system keeps the concrete spread out without using chemical slow-downs that hurt early strength development.
(1). Key Physical and Chemical Characteristics
The monomer looks like white to off-white flakes and has a solid content of more than 98%, which means that moisture won't get in the way of PCE production very much. The amount of hydroxyl it has is between 22 and 28 mg KOH/g, and its pH stays stable in water between 5 and 7. The level of unsaturation is ≥0.35 mmol/g, which means that copolymerization with acrylic acid will work well during production. The moisture level stays below 0.2%, which stops premature hydrolysis that would lower the efficiency of polymerization.
This monomer stands out because it keeps more than 95% of its double bonds. This standard is important because it has a direct effect on how well the monomer joins with the PCE backbone during synthesis. Lower retention rates cause reactions to stop before they're finished, which wastes raw materials and makes the performance of the admixture unpredictable.
(2). Performance Benefits Across Climate Zones
Working with concrete is more than just reducing the amount of water it needs. In tropical areas with temps above 35°C, regular superplasticizers stop working in just 60 minutes because they lose their ability to make things workable because of faster hydration processes. The long molecular chains of this monomer make a barrier around the cement particles that stops heat from speeding up.
Large-scale building projects show what the effect of HPEG 2400 Extended Slump Retention Monomer is in real life. For long periods of time, continuous placement is needed for mass concrete pours for dam foundations or high-rise raft slabs. Chemical retarders or secondary doses are used in traditional methods, which make things more complicated and increase the risk of harm. This monomer keeps its high flowability during pours that last for hours, and it also supports low-heat hydration profiles that are necessary to keep thermal cracking from happening.
- HPEG 2400 vs Other Slump Retention Monomers: Making the Optimal Choice
When the admixture business makes choices about what to buy, they weigh technical success against the total cost of ownership. When you look at the different molecular weights, you can see why the 2400 specification is so important.
(1). Superior Hot Weather Resistance
Monomers with a lower molecular weight, usually between 1800 and 2000, are good at removing water but have trouble keeping it when heated up. When heat increases the speed at which particles collide, their shorter side chains don't provide enough steric safety. On the other hand, molecular weights above 3000 can cause over-retardation, which can delay setting times and mess up building plans.
The best balance is reached at a molecular weight of 2400. In Southeast Asian markets where the temperature reached 38°C, tests showed that concrete could keep its slump values above 180mm for three hours without needing to be dosed again. For similar formulas using 2000 molecular weight monomers to be workable, they needed extra amounts after 90 minutes.
(2). Cement Compatibility and Formulation Flexibility
Different types of cement have different mineral makeup that affect how well admixtures work. High C3A cements are common in some markets, and they harden quickly, using up the superplasticizer's effectiveness very quickly. The longer side chains of this monomer can buffer against these changes, making the performance more consistent across different cement sources.
This is a big problem for concrete producers who serve more than one market. If a recipe is designed for one type of cement, it might not work with other providers. This sensitivity is lowered by HPEG 2400 Extended Slump Retention Monomer, which lets makers keep mix designs the same even when raw materials change. This freedom leads to better operations and fewer requests for technical help.
(3). Long-Term Value Considerations
When procurement teams look at monomer options, they need to look at more than just the cost per ton. They need to look at the total value delivered. Lower intake rates because of better efficiency often cancel out price increases that seem to be there. When concrete stays workable without extra dosing, it saves money on labor and makes the job better. Rejected loads because they don't slump enough are a huge waste of resources that don't save any raw materials.
This economics is shown by field data from ready-mix operations in the Middle East. When businesses moved to monomers with a higher molecular weight, customer complaints dropped by 60% during the busy summer months. The extra cost of the monomer was dwarfed by the cost of dealing with complaints, refused loads, and damage to the company's image.
- Procurement and Supply Chain Insights for HPEG 2400
More than just technical proof is needed to add new raw materials to production processes. If lab success can be turned into a business, it depends on how reliable the supply chain is, how well the logistics work, and how well the regulations are followed.
(1). Manufacturing Capacity and Delivery Assurance
EverStar Group runs production facilities that can make more than 50,000 tons of HPEG 2400 Extended Slump Retention Monomer goods a year, and they keep a strategic inventory of 5,000 tons or more. This scale is important when production plans are thrown off by sudden increases in demand or when trying new recipes needs quick sample iteration. Our facilities are close to major ports, which cuts down on transportation costs and gives us more control over shipping plans.
The minimum order quantity is 5 tons, which lets medium-sized makers try out the monomer without having to commit to too much inventory. Standard products are sent out within three days, while customized orders that include specific purity needs or packaging preferences are sent out within five to seven days.
(2). Regulatory Compliance and Documentation
For international business to run smoothly, all regulations must be aligned. The monomer is registered with EU REACH, which makes it easy to sell in all European markets.
- Certifications including ISO and GCC standards make sure that the products work with regional building rules. Halal and KOSHER certifications help with sales in places where religious rules must be followed.
Each shipment comes with full paperwork packages that include Safety Data Sheets (SDS) in several languages, Certificates of Analysis (COA) that show test results specific to the batch, and Technical Data Sheets (TDS) that explain how to use the product. Third-party testing through SGS and Intertek gives customers who want extra assurance an independent check.
(3). Flexible Commercial Terms
Managing cash flow is hard when you're buying from businesses. We offer different ways for buyers to pay, such as letters of credit for first-time customers and longer terms for partners we've worked with before. This adaptability comes from the fact that building ties with suppliers means dealing with different business and banking systems.
Packaging choices include 25 kg bags for lab tests, intermediate bulk containers (IBC), and bulk tanker shipments for large-scale operations. This freedom means that big customers don't have to waste packaging, and small users can still easily handle the product.
- Application Methods and Best Practices for Using HPEG 2400 in Concrete
Technical details don't mean much if they can't be put into practice. To successfully deploy this monomer, you need to know how it works with current PCE synthesis methods and concrete mix designs.
(1). PCE Synthesis Parameters
The monomer and acrylic acid copolymerize in a controlled way. Aqueous solution polymerization at temperatures between 60°C and 90°C, using peroxide or persulfate as initiators, is a common way to make things. Because it keeps a lot of double bonds, it's easy to incorporate into the polymer backbone, which cuts down on the waste of unreacted monomers.
The molecular amounts of the monomer and acrylic acid need to be tweaked based on how well the concrete is supposed to work. A higher monomer level makes the slump last longer, but it may slow down the initial water loss. Combining HPEG 2400 Extended Slump Retention Monomer with lower molecular weight variants in mixing methods makes mixes that are good at both spreading right away and being workable for a long time.
(2). Concrete Mix Design Integration
Dosage rates for additives usually fall between 0.15 and 0.40% by weight of cement. These rates can change depending on the type of cement, the water-to-cement ratio, and the desired performance. For high-strength concrete mixes (C60–C80 grades), bigger doses are often needed to get the workability needed while keeping the water level low.
The settings used for testing should be the same as those at the real spot. When tested in the lab at 23°C, a product may work fine, but it won't in the field at 35°C. Simulated testing at high temperatures gives accurate predictions of performance, which keeps expensive fails from happening in the field. EverStar Group provides research and development support 24 hours a day, 7 days a week to help improve formulations for different regions, types of cement, and performance needs.
(3). Troubleshooting Common Challenges
When high molecular weight monomers are mixed with some types of cement or extra cementitious materials, excessive delay can happen. This shows up as setting being delayed for too long of a time. Some solutions are to change the amounts of monomers and acids, add small amounts of admixtures that speed up the process, or mix with monomers that have a lower molecular weight.
When monomer standards change from batch to batch, there are worries about consistency. When molecular weight variations are outside of certain ranges (2400±100 g/mol), concrete behaves in ways that are hard to predict. Performance consistency is maintained by strict quality control at the supplier level, which includes iodine value testing for double-bond confirmation and experimental synthesis trials.
- Why Choose HPEG 2400? The Rational Choice for High-Performance Concrete Solutions
The strategic choice of raw materials affects both the efficiency of production right now and the company's place in the market in the future. This monomer is the best choice for forward-thinking companies that make concrete additives for a number of reasons.
(1). Technical Performance Consistency
Because the monomer is chemically stable and has precise molecular weight control, the behavior of the concrete can be predicted. Producers who want to build a reputation in their region for dependable workability need raw materials that work the same way no matter what the season is or how much cement is available. In mature markets where customers expect guarantyd performance, this dependability becomes a way to stand out from the competition.
(2). Supplier Partnership Value
Getting raw materials is more than just making purchases. The ability to provide technical help has a big effect on how well an implementation goes. The in-house labs at EverStar Group help customers find the best synthesis conditions for their equipment and target markets by creating custom formulations. Before committing to large-scale production, free samples can be used to test the product with local aggregates and cements.
Our multilingual technical team is available 24 hours a day, seven days a week, across all time zones to answer questions about synthesis, fix performance problems, and give advice on how to make the best use of mix designs. When entering new markets or making specific concrete Applications, this service framework is very helpful.
(3). Sustainability and Future-Readiness
Environmental responsibility is becoming more and more important in the construction industry. Because the monomer works so well, less chemical is used per cubic meter of concrete. Longer workability cuts down on rejected batches and waste. EverStar Group has promised to cut carbon emissions by 30% by 2030. This is in line with customer sustainability efforts and supports LEED certification and green building projects.
Research and development spending (5% of annual income) makes sure that products are always getting better and new ones are being made. As building technology moves toward more durable and high-performance concrete, our innovation pipeline helps customers adapt to new market needs.
-Conclusion
The main task of HPEG 2400 Extended Slump Retention Monomer is to keep the workability of concrete high under tough conditions without affecting its strength development. Its molecular architecture has been adjusted to provide longer slump retention through steric hindrance processes instead of chemical retardation. This technical approach works especially well for ready-mix businesses that deliver over long distances, work in hot climates, or make high-performance concrete. It can be a strategic raw material that helps concrete producers set their products apart and solve customer problems that generic admixtures can't. This is possible when they have reliable supply chains, full technical support, and strict quality control.
FAQ
(1). Why choose 2400 molecular weight specifically for tropical construction applications?
The 2400 molecular weight makes the polyether side chains longer, which makes it harder for cement particles to move around. This molecular structure doesn't react quickly to water loss that happens in high-temperature environments. It stays workable for 180 minutes or more, even when the temperature outside is above 35°C. Lower molecular weights don't protect well enough against thermal stress, and higher weights risk setting too slowly.
(2). Does extended slump retention affect early concrete strength development?
When mixed correctly, this monomer makes the material easier to work with by spreading out physically instead of chemically slowing it down. The compression strengths after 24 hours are still about the same as with regular additives, and the strengths after 7 days and 28 days meet or beat the design standards. The key is to use the right amount and make sure that the recipe balances with other PCE components.
(3). How does storage stability impact monomer performance?
It is important for keeping stability that the moisture level is less than 0.2%. The monomer should stay in buildings that are cool, dry, and well-ventilated in cases that are tightly sealed. Humidity can cause hygroscopic absorption, which can cause caking and even premature breakdown. Material that is stored properly will keep working the same way for a year, but containers that have been opened should be used right away.
- Partner with a Trusted HPEG 2400 Extended Slump Retention Monomer Manufacturer
EverStar Group has 14 years of experience making specialized goods and has the production scale and technical skills that mid-sized admixture makers need. When you buy from Our Factory directly, there are no markups added by middlemen. This saves you 20–40% on costs compared to buying through distributors, and our high quality standards are confirmed by ISO and REACH Certifications. You are welcome to ask for free samples so that we can test their compatibility with your cement sources and mix designs. Our team will work with you to find the best synthesis settings and concrete formulas so that the project goes smoothly. Get in touch with info@cneverstar.com right away to talk about your specific slump retention problems and find out how our HPEG 2400 Extended Slump Retention Monomer supplier can help you reach your production goals. You can find full technical specs, case studies, and resources you can download at cneverstar.com.
References
1. Fang, Y., et al. (2023). Study on dispersion, adsorption, and hydration effects of polycarboxylate superplasticizers with different side chain structures in reference cement and belite cement. Materials, 16(11), 4168.
2. Li, Z. K., & Peng, J. H. (2013). Adsorption behavior of polycarboxylate superplasticizer on cement particles. Applied Mechanics and Materials, 405–408, 2834.
3. Lv, S. H., Gao, R. J., & Duan, J. P. (2011). Effects of chemical structure on adsorption of polycarboxylate superplasticizers on cement particles. Applied Mechanics and Materials, 80–81, 185–189.
4. Liu, Y., et al. (2018). Effect of molecular weight of slow-release polycarboxylate superplasticizer on the properties of cementitious system. Advances in Cement Research, 30(7), 285–291.
5. Lv, S. H., Li, D., & Cao, Q. (2012). Study on relationship between structure and properties of polycarboxylate superplasticizer. Advanced Materials Research, 487, 43.
6. Gao, R. J., Lv, S. H., & Cao, Q. (2012). Effects of polycarboxylate superplasticizers on hydration and microstructure of hardened cement paste. Advanced Materials Research, 487, 692–696.
Complete Guide to TPEG 2400 Low-Temperature Fluidity Monomer
When cold weather threatens your concrete projects with slump loss and poor workability, TPEG 2400 Low-Temperature Fluidity Monomer emerges as the engineered solution. This specialized macromonomer maintains molecular flexibility at temperatures as low as -15°C, ensuring polycarboxylate superplasticizers deliver consistent dispersion performance throughout winter construction. Unlike conventional PCE monomers that stiffen and lose effectiveness below 10°C, this ~2400 molecular weight compound features optimized ethylene oxide chains that prevent viscosity increases, allowing concrete to remain pumpable and workable without auxiliary heating systems.
- Understanding TPEG2400 Monomer: Properties and Characteristics
This cold-weather macromonomer is unique in the way it is made chemically, which makes it useful for making concrete admixtures. The product is mostly made up of white to off-white flakes whose molecular weight is carefully kept at about 2400 daltons. In cement paste systems, this particular chain length strikes a good mix between hydrophilic performance and steric blocking effects.
(1). Chemical Identity and Molecular Structure
This monomer can be found in world chemistry databases by its CAS‑31497‑33‑3. Polyoxyethylene chains that end in reactive vinyl groups make up its molecular backbone. The unsaturation level staying at or above 0.35 mmol/g is what makes this structure so useful; this is a number that directly relates to how well polymers are formed. Your team's copolymerization of this monomer with acrylic acid turns those double bonds into anchor points for making the PCE backbone. The hydroxyl number between 22 and 27 mg KOH/g shows that the ethylene oxide addition process is being carefully controlled. This stops any unwanted branches that could hurt the performance at low temperatures.
(2). Physical Properties and Performance Indicators
If the solid content is more than 98%, there will be little to no moisture interference during storage and processing. This high level of purity saves your batch stability because water contamination can cause polymerization or hydrolysis to happen too soon. A 5% water solution has a pH between 5.0 and 7.0, which means it can work with alkaline cement environments without speeding up the hydration reactions. The ethylene oxide segments in this monomer can still move around when the temperature drops to 5–10°C. When the same conditions are applied to standard HPEG or VPEG alternatives, the chains become stiffer, which makes it harder for the particles to stick to them. This makes a direct difference between mixes that need mechanical vibration or hot water additions to work and ones that work easily through dense rebar congestion.
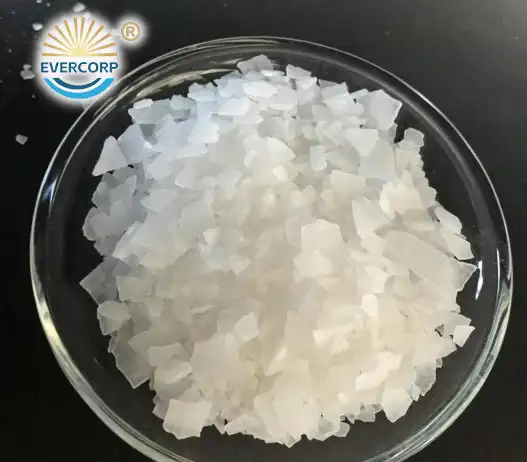
(3). Safety and Quality Compliance Standards
The factories that make this macromonomer have to meet strict worldwide approval standards. To get into the European market, REACH compliance makes sure that all of the materials used go through a thorough toxicological evaluation. ISO 9001 approval proves that differences between batches stay within accepted limits. There are three tests that are done on every production run: iodine value testing to make sure the double bonds stay together, gel permeation chromatography to make sure the molecular weight distribution is correct, and Karl Fischer titration to make sure the moisture content is less than 0.3%. These quality control steps are important because even small changes in hydroxyl value or unsaturation can have big effects on how well the final PCE works in winter concrete Applications.
- Comparing TPEG2400 with Other Low-Temperature Fluidity Monomers
To choose the best macromonomer for making concrete in cold climates, you need to know how different molecular structures react to temperature stress. A number of options are available on the market, and each one has its own pros and cons.
(1). TPEG2400 Versus TPEG1000 Molecular Weight Variants
The molecular weight of TPEG 2400 Low-Temperature Fluidity Monomer has a big effect on how PCE side chains connect with cement particles. The 1000 dalton version has shorter ethylene oxide chains that allow for fast initial diffusion but not much slump retention. Your concrete becomes workable right away, but it stops being wet in 45 to 60 minutes. The 2400 molecular weight version makes those side chains longer, which makes the steric repulsion forces stronger and keeps particles apart for 90 to 120 minutes. This longer workability window keeps the mix from stiffening too soon when it has to be transported over distances of more than 30 kilometers. The longer chains also have lower glass transition temperatures, which means that molecules can still be flexible even when the temperature outside is getting close to freezing. Contractors who work in Alaska or northern Canada depend on this property to get rid of the need for heated water, which makes their jobs more difficult and costs more in energy.
(2). Performance Benchmarks in Cold Environment Testing
At room temperature (5°C), tests done in the lab show that the different types of monomers are different in ways that can be measured. When compared to baselines at room temperature, concrete mixed with standard HPEG-based PCE has 15-20% less slump retention. When this specialized macromonomer is added to the same mixture, it keeps 95–98% of its original flow properties. Using rotational viscometers for rheological testing shows that yield stress only rises by 8–12% at 5°C, while it rises by 35–40% for regular monomers. During overnight curing at temperatures dropping toward -5°C, formulations based on this low-temperature platform maintain flowability and workability, helping concrete remain pumpable without heated mixing water.
(3).Selection Criteria for Application-Specific Requirements
Which of the available monomers to use depends on a number of project factors. The 2400 molecular weight choice is best for building infrastructure in the Nordic areas where winter temperatures stay below 0°C. Seasonal building in climates that are changing might work better with smaller molecular weight options when the weather is nicer. For high-strength concrete uses that need water-to-cement ratios below 0.35, longer ethylene oxide chains are needed for better dispersion. For building uses, self-compacting concrete needs to have stable rheology throughout placement. The longer side chains stop segregation and bleeding, which would lower the quality of the surface finish. By comparing these factors to your unique production needs, you can find the most cost-effective option without putting too many limits on the material's performance.
- Procurement Considerations for TPEG2400 Monomer
It takes more than just comparing prices to find a reliable source of this specialized macromonomer. Strategic procurement strikes a balance between making sure quality, making sure deliveries go smoothly, and following the rules.
(1). Direct Manufacturer Versus Distributor Sourcing
There are a number of good reasons to buy chemicals straight from the makers. You can get help from expert support teams that know about the processes of polymerization and the rheology of concrete. These experts can look at GPC traces and iodine values to find out why batch performance changes in ways that aren't expected. With factory-direct connections, you can also change the hydroxyl values or molecular weight ranges to fit the minerals in your area. Distributor networks make it easy to get products in different areas and let you order smaller amounts for testing purposes. On the other hand, there isn't a lot of technical detail and there may be problems with authenticity because fake or weakened materials sometimes make their way into developing market sales channels.
(2). Order Quantities and Lead Time Management
Trial orders of TPEG 2400 Low-Temperature Fluidity Monomer usually begin with shipments of one metric ton, which is equal to about 40 bags of 25-kilogram packaging. This amount lets you do full pilot-scale tests without spending a lot of money. For production-scale purchases, orders must be at least five metric tons in order to justify the logistics of shipping them in containers. Companies that use more than 100 metric tons a year should talk about dedicated production campaigns. These agreements lock in better prices and guarantee monthly allocations during the busiest demand times in the winter. Lead times depend on how busy the supplier is and where the goods are being shipped from. Standard items from a well-stocked warehouse usually ship within three days. It takes five to seven days to synthesize and check the quality of molecules with specific molecular weight requirements or hydroxyl value changes.
(3). Certification Requirements and Sample Protocols
Every package needs to come with the right paperwork to make sure it gets through customs and that the quality can be tracked. Safety Data Sheets, Certificates of Analysis, and Technical Data Sheets are available in more than one language from suppliers who follow REACH rules. Third-party testing reports from independent laboratories such as SGS or Intertek provide additional confirmation of claimed specifications. Before making big purchases, ask for 0.5 to 1 kilogram samples to make sure they are compatible. Check those samples against the cement sources and gravel grades that you use. The performance can vary a lot depending on the raw materials that are available in your area. Reliable sellers give these samples away for free because they know that technical proof lowers the risk of doing business for both parties.
- Trusted Suppliers and Brands of TPEG2400 Monomer
Finding trustworthy sources for macromonomers that are found in cold climates protects the quality of your production and the continuity of your supply chain. There are a number of things that set exceptional suppliers apart from commodity vendors.
(1). Global Manufacturer Profiles
EverStar Group has several industrial sites in the southern, eastern, and northern regions. These facilities can hold more than 5,000 tons of inventory. Since we started making chemicals in 2012, 14 years ago, we help people in more than 50 countries make concrete admixtures. Some of the Fortune 500 companies and major construction material companies, like CEMEX and CHT, are among our clients. Being close to major ports lowers logistics costs and speeds up the loading of containers—standard shipments leave within 72 hours of order confirmation. Our network of facilities can produce more than 50,000 tons of goods every year, and we put 5% of our profits back into research and development. This dedication leads to constant improvements in molecular design and the efficiency of synthesis.
(2). Verification of Authorized Distribution Networks
In specialized chemistry markets, fake products really do pose a threat. Unauthorized sellers may mix real goods with cheaper ones to weaken them or lie about hydroxyl values by falsifying paperwork. Protect your business by checking the credentials of your suppliers in a number of different ways. Check that the Certifications being claimed match the records of the relevant authorities. The European Chemicals Agency website can be used to confirm REACH registration numbers. Ask current customers who have used similar applications to give you references. Reliable suppliers are happy to put potential customers in touch with current customers so that the customers can talk about how quickly the technical support team responds and how consistent the batches are. Check to see if suppliers offer full service packages that go beyond just delivering products. Support in multiple languages and availability 24 hours a day, seven days a week shows a strong dedication to customer success. Offering mixing tools, how-to videos, and on-site training shows knowledge that commodity buyers can't copy.
(3). Long-Term Partnership Benefits
Building long-term ties with TPEG 2400 Low-Temperature Fluidity Monomer suppliers has benefits that transactional buying can't beat. Account managers are dedicated to learning about your specific production problems and making suggestions for changes to the formula as cement sources change with the seasons. Priority distribution during supply constraints makes sure that your production keeps going even when spot market access drops. Through collaborative development programs, you and other people can work together to make molecular weights or unsaturation levels that are best for the weather in your area. Our team can help you come up with OEM and ODM formulas, and we can also customize the packaging to fit your brand's style. Logistics tracking tools let you see the state of shipments in real time, so unexpected delays don't stop production. These parts of a partnership give you a competitive edge that goes far beyond just buying chemicals.
- Practical Applications and Case Studies of TPEG2400 in Polymers
Real-world performance data shows that this specialized macromonomer solves common construction problems that come up in cold weather for a wide range of project types.
(1). Cold-Climate Infrastructure Development
Putting down concrete for a high-speed rail project in northern Canada was hard from October to March, when the temperature regularly dropped to -10°C. In the past, PCE formulations needed systems for heating mixing water, which used a lot of energy and made running a batch plant more difficult. When the low-temperature macromonomer was changed to a polycarboxylate superplasticizer, there was no need for any heating at all. Even though it was -8°C outside, the concrete kept its 210mm slump for 90 minutes after it was mixed. The increase in compressive strength was the same as the baseline performance in the summer, reaching 35 MPa after seven days. The project cut down on extra heating costs and sped up building by six weeks. For example, crews kept filling foundations all through November, when in the past winter shutdowns would have stopped work.
(2). High-Strength Self-Compacting Concrete Applications
Self-compacting concrete that could flow through crowded support in densely packed shear wall sections was needed for building tall buildings in Stockholm. Different changes in temperature between morning and afternoon (8°C in the morning and 18°C in the afternoon) made it hard to keep things consistent. When PCE was made with standard monomers, the flow table spread changed by 25% over that temperature range. Using this cold-adapted macromonomer in a new formulation cut flow variation to less than 8%. Intricate formwork was filled with concrete that didn't move at all, so there were no bug holes and the finish quality was good enough to be used straight off the forms. The stable rheology across temperature changes cut down on waste from rejected batches and made it easier to predict the surface finish.
(3). Extended-Distance Ready-Mix Transport
A regional ready-mix company that worked with rural construction sites had to deal with average delivery times of 90 minutes from the plant to the site. Deliveries went well in the summer, but temperatures between 10 and 15°C in the spring and fall caused too much slump loss. It was common for concrete to not be easy to work with when it came, so water had to be added, which weakened its strength and sturdiness. The working time was increased by 40 minutes when PCE made from the 2400 molecular weight monomer was used. When drivers got to remote sites, they always brought concrete that still had 180–200 mm of slump, so there was no need for field water additions. There was a noticeable rise in customer satisfaction, and the manufacturer took market share away from competitors who were still having problems with performance in cold weather.
- Conclusion
The TPEG 2400 Low-Temperature Fluidity Monomer solves the concrete industry's long-standing problems with cold-weather performance by carefully designing its molecular structure. Its about 2400 molecular weight ethylene oxide chains stay flexible at temperatures where most monomers become hard and stop working. To be successful in buying, you need to know about the following specifications: solid content above 98%, unsaturation above 0.35 mmol/g, and hydroxyl values between 22 and 27 mg KOH/g. When you compare this macromonomer to others like TPEG1000, you can see that it performs better in terms of keeping its shape and being fluid at low temperatures. Buying from certified makers makes sure that you follow the rules and gives you access to expert help that you can't get from commodity sellers. Real-life case studies show measurable benefits, such as no longer having to pay for heating, stable rheology even when temperatures change, and longer working times for long-distance transport.
- FAQ
(1). What minimum order quantity applies to TPEG2400?
For first-time sales, the standard minimum order quantity is one metric ton, which is equal to 40 bags of 25-kilogram packing. This amount allows for full pilot-scale testing of a number of different concrete mix designs. For production-scale purchases, the minimum weight needed to justify shipping costs in a container is usually five metric tons. Companies that use more than 100 metric tons of the product each year should look into dedicated production campaign agreements that lock in prices and guarantee monthly allocations during the busiest winter months. Suppliers also offer free samples weighing 0.5 to 1 kilogram for testing how well they work with your chosen cement sources and material grades.
(2). How does molecular weight affect cold-temperature performance?
The ethylene oxide chain length is directly affected by molecular weight. This length affects the steric forces that push cement particles apart. The 2400 molecular weight version has longer side chains that keep particles apart for 90 to 120 minutes, even when the temperature outside is 5°C. Shorter versions with 1000 molecular weight spread out quickly at first, but they don't hold their shape well—concrete loses its fluidity in 45 to 60 minutes. Longer chains also have lower glass transition temperatures, which means that molecules can still be flexible when the temperature is getting close to freezing. This feature gets rid of the need for hot water in cold places, which makes operations simpler and uses 30–50% less energy.
(3). Can this monomer blend with existing HPEG formulations?
Different macromonomers can work together if their chemical structures and how fast they polymerize are similar. During transitional times, gradual replacement lets you see how performance has changed without having to completely change the formulation. Adding 20 to 30 percent of this special monomer to HPEG-based systems that are already in use can often make them more fluid at low temperatures while keeping the same processing parameters. To get the best molecular weight distribution in the final PCE, acrylic acid ratios and polymerization conditions usually need to be changed for full replacement. This process can be sped up by asking your seller for technical help. Formulators with a lot of experience can suggest starting ratios based on your cement's reaction and how well you want the concrete to work.
- Partner with EverStar Group for Cold-Climate Concrete Solutions
EverStar Group sells TPEG 2400 Low-Temperature Fluidity Monomer directly from the factory. They offer 14 years of experience making chemicals and full technical support. Our three regional production sites keep more than 50,000 tons of yearly capacity and keep 5,000 tons of stock on hand to make sure we have a steady supply during the busiest winter months. We follow international quality standards and our products are supported by REACH compliance and ISO 9001-certified processes, with third-party testing available from SGS or Intertek. In addition to supplying products, we also create OEM and ODM formulas and offer free samples for testing with your local aggregates every day. Our technical support is available 24/7 in multiple languages. Contact info@cneverstar.com or visit cneverstar.com right now to get your Certificate of Analysis and Technical Data Sheet and talk about how our cold-climate macromonomer can help you make more winter concrete while using less energy and working longer.
- References
1. Plank, J., Sakai, E., Miao, C. W., Yu, C., & Hong, J. X. (2015). Chemical admixtures—Chemistry, applications and their impact on concrete microstructure and durability. Cement and Concrete Research, 78, 81–99.
2. Li, Y., Yang, C., Zhang, Y., Zheng, J., Guo, H., & Lu, M. (2014). Study on dispersion, adsorption and flow retaining behaviors of cement mortars with TPEG-type polyether kind polycarboxylate superplasticizers. Construction and Building Materials, 64, 324–332.
3. Xie, Y., et al. (2023). Understanding the temperature-dependent workability of cement paste with polycarboxylate superplasticizer. Journal of Building Engineering, 76, 107408.
4. Winnefeld, F., Becker, S., Pakusch, J., & Götz, T. (2007). Effects of the molecular architecture of comb-shaped superplasticizers on their performance in cementitious systems. Cement and Concrete Composites, 29(4), 251–262.
5. Puertas, F., Santos, H., Palacios, M., & Martínez-Ramírez, S. (2005). Polycarboxylate superplasticiser admixtures: effect on hydration, microstructure and rheological behaviour in cement pastes. Advances in Cement Research, 17(2), 77–89.
6. Lei, L., & Plank, J. (2014). Synthesis and properties of a vinyl ether-based polycarboxylate superplasticizer for concrete possessing clay tolerance. Industrial & Engineering Chemistry Research, 53(3), 1048–1055.
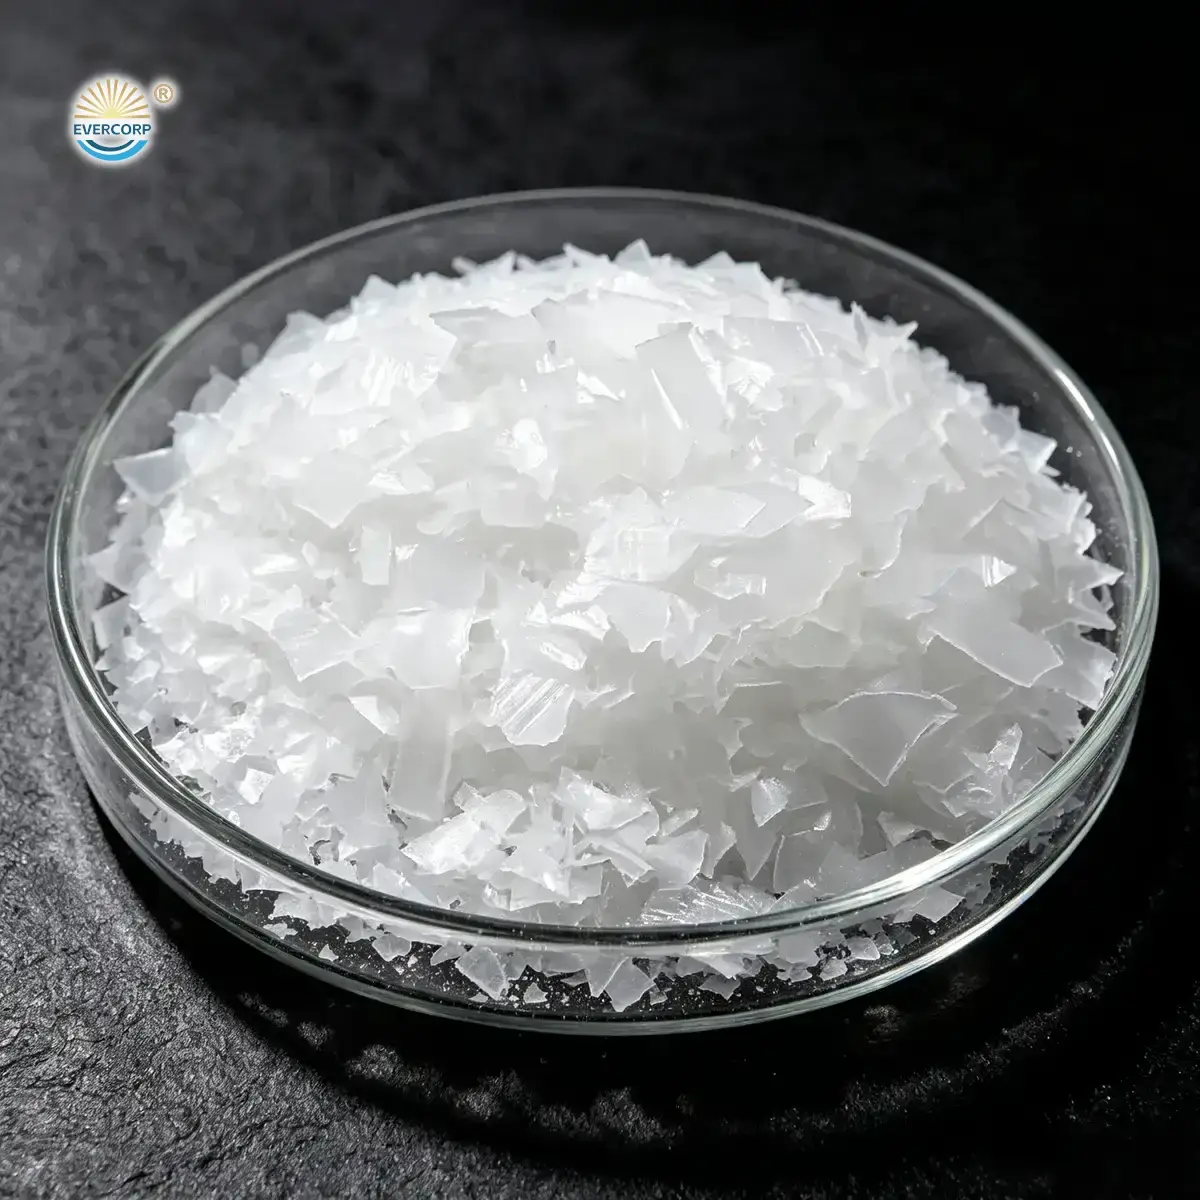
What is a Polycarboxylate Ether Monomer used for?
Polycarboxylate Ether Monomer serves as the foundational raw material for synthesizing high-performance polycarboxylate superplasticizers (PCE) used primarily in concrete admixtures. This unsaturated polyether—including variants like HPEG, TPEG, and EPEG—enables concrete manufacturers to achieve superior water reduction (25-35%), extended slump retention (1-2 hours), and enhanced workability. When polymerized with acrylic acid, the resulting PCE superplasticizer disperses cement particles effectively, reducing viscosity and allowing concrete to flow smoothly through dense reinforcement and reach extreme pumping heights without compromising structural integrity.
Understanding the Chemistry Behind PCE Monomers
The unique structure of these monomers is what makes them work technically. A Polycarboxylate Ether Monomer has a comb-like structure at its center, with hydrophilic polyoxyethylene (PEO) side chains stretching from a reactive backbone that has double bonds. This design produces a two-way mechanism: the backbone's carboxyl groups attach to cement particles through electrostatic binding, and the long PEO side chains create steric hindrance, which keeps particles physically apart and stops flocculation. Molecular weight, which is usually between 2400 and 4000 g/mol, has a direct effect on the balance between how well water is removed and how long the slump lasts.
Key Chemical Parameters That Define Performance
When manufacturers buy things, they should pay attention to three important features. Unsaturation degree, which is given in mmol/g, shows how many reacting double bonds are available for polymerization. Higher numbers mean better conversion rates and better ability to remove water. The hydroxyl value (22–28 mg KOH/g) shows that the polyether chain is pure and full, and the solid content above 98% makes sure that there isn't too much moisture that could cause caking during storage or mess up the processes that happen during synthesis. Gel permeation chromatography (GPC), iodine value titration, and Karl Fischer analysis are used to test these factors thoroughly and make sure that they are consistent from batch to batch, which is what production lines need.

How Molecular Structure Drives Concrete Performance
When the monomer is turned into PCE superplasticizers, its side-chain length and density can be changed to change how the concrete behaves. Longer side chains (3000–4000 MW) provide better steric resistance, which is very helpful for keeping the workability during long-distance shipping in hot regions or long mixing cycles. Shorter chains (2000–2400 MW) focus on quick dispersion and early strength development, which makes them perfect for precast operations that need to turn over forms quickly to make money. Because these properties can be fine-tuned, manufacturers can match them to specific types of cement, aggregates, and jobsite conditions. This is something that traditional naphthalene-based admixtures can't do.
Primary Industrial Applications Driving Global Demand
Most Polycarboxylate Ether Monomer are used in the Construction Chemicals industry. This is because infrastructure growth and urbanization are driving these trends. When concrete has to be pumped up to 300 meters in height through small pipes, it's a very difficult job for high-rise building projects. When standard monomers are turned into PCE admixtures, they greatly lower the density of the plastic. This lets it flow smoothly under high pressure, without clogging or segregating pipes. In cities like New York, Singapore, and Mumbai, where building skyscrapers depends on reliable pumping technology to stay on schedule, this ability has become essential.
Precast Concrete Manufacturing Benefits
There are a lot of time and quality stresses on precast companies. Because the monomer helps the material gain strength quickly, manufacturers can strip forms in 12 to 16 hours instead of the usual 24 hours. The controlled decrease of water is what speeds things up—less mixing water means faster hydration kinetics and earlier load-bearing ability. At the same time, the admixture stays flexible enough to fill the mold completely, even when the geometry is complicated and there are a lot of rebar arrays. Plants say they can increase throughput by 30–40% without lowering the quality of the finish or the accuracy of the measurements. This has a direct effect on their bottom line in competitive regional markets.
Self-Compacting Concrete and Specialized Uses
Self-compacting concrete (SCC) mixtures need to be able to flow very well while also being resistant to segregation. Polycarboxylate ethers do a great job of meeting this seemingly contradictory need. The synthesized PCE makes it possible for concrete to flow into complex shapes just by gravity. This means that there is no need for mechanical vibration, which can damage utilities that are embedded or sections with thin walls. SCC is being used more and more in infrastructure projects like tunnels, bridges, and marine structures because it can completely consolidate around complex reinforcement patterns. In addition to construction, the monomer's dispersing properties are being used in new coatings and adhesives products, though these are still small market segments compared to concrete admixtures.
Comparing Performance Against Alternative Chemistries
Before Polycarboxylate Ether Monomer technology came along, the market was controlled by traditional naphthalene formaldehyde superplasticizers. Naphthalene-based goods are cheaper per ton, but they need higher dosage rates (0.8–1.2% of the cement weight vs. 0.2–0.5% for PCE) and only reduce water by 15-20%. The slump retention window doesn't last longer than 45 minutes, so ready-mix manufacturers have to add retarders, which makes quality control harder. Polycarboxylate ethers get rid of these problems by providing better initial dispersion and longer-lasting workability. This means that trucks can get to faraway job sites without having to worry about slump loss. The total cost per cubic meter of concrete often favors PCE, even though it costs more for the raw materials. This is especially true in cities where travel times are longer than an hour.
Evaluating Purity Grades and Quality Standards
From 95% to 99% solid content, different suppliers offer different purity grades that purchasing managers have to deal with. The 3-4% change has a big effect on activities further down the line. When the purity is lower, water and polyether oligomers are introduced, which slow down the polymerization process and make the end PCE performance vary from batch to batch. Manufacturing companies can tell this by the fact that buyers of ready-mix concrete often complain and the slump results aren't always the same. Setting quality standards for unsaturation levels above 0.35 mmol/g and hydroxyl levels between 22 and 28 mg KOH/g lowers the chance of buying the wrong thing. Certifications like REACH, ISO 9001, and ASTM compliance give you even more peace of mind, but lab checking of sample runs is still the best way to be sure before signing large-volume contracts.
Strategic Procurement Considerations for Manufacturers
Finding polyether monomers means figuring out how to get around regional production hubs and transportation networks. China has most of the world's supply and has lower costs because its petrochemical infrastructure is linked. However, the quality of products from smaller makers needs to be carefully checked out. European and North American suppliers usually charge more, but their standards are always the same and follow strict environmental rules. The choice between direct factory sourcing and working with a distributor depends on how much you need to buy. Producers who need 200 to 600 tons of goods a year can usually save 20 to 40 percent by going direct to the factory instead of going through a middleman, as long as they can meet the minimum order quantities, which start at 5 tons.

Managing Lead Times and Inventory Strategy
Standard-grade monomers can be shipped within three to five days if the manufacturer keeps an inventory on hand. For customized molecular weights or functionalized variants, lead times are longer, taking seven to ten days for synthesis and quality testing. Plants that use lean inventory models have to weigh the costs of keeping inventory against the risks of supply chain disruptions. One important thing to look at when evaluating a seller is how much inventory they have on-site. For example, makers who keep 500 tons or more in stock can protect themselves against production spikes or shipping delays. It doesn't matter how close a factory is to a port; being close to a major shipping hub lowers freight costs and the chance of damage during transit, especially when working with flake materials that break down when exposed to moisture during long inland transport.
Documentation and Compliance Requirements
For international trade in Polycarboxylate Ether Monomer specialty chemicals, you need to keep a lot of paperwork. Before starting trials, procurement teams should ask for Certificates of Analysis (COA), Technical Data Sheets (TDS), and Safety Data Sheets (SDS). For markets in the US and Europe, REACH registration numbers and FDA compliance letters make it easy to get goods through customs. Halal and Kosher approvals are becoming more common for producers of chemicals to the Middle East and other specialized markets, but they are not as common for Industrial Chemicals. Third-party testing reports from SGS or Intertek provide independent confirmation of claimed specifications. This gives supplier qualification audits more weight. These papers are also very helpful for figuring out problems with field performance because they set the standard for quality for forensic research.
Why Does EverStar Group Stand Out in the PCE Monomer Market?
The manufacturing skills of EverStar Group combine size with technical accuracy. Our three strategically placed production facilities, in the Southern, Eastern, and Northern regions, make more than 50,000 tons of product every year. This makes sure that we always have enough, even during busy construction seasons. With an unsaturation level above 0.35 mmol/g and a molecular weight control of about 2400 g/mol, the polymerization kinetics are reliable, which is what PCE makers need for stable batch production. Keeping more than 5,000 tons of inventory on-site keeps competitors who use just-in-time manufacturing models from having to deal with supply problems.
Quality assurance is more than just meeting basic requirements. Every production batch goes through strict GPC analysis to make sure the molecular weight distribution is correct, iodine titration to make sure the double bonds stay in place, and Karl Fischer testing to make sure the moisture content is less than 0.2%. This three-check method, along with REACH, ISO 9001, and ASTM C494 approvals, has earned the trust of large admixture manufacturers. The company's 99.5% on-time delivery record to more than 50 countries shows managerial excellence that smaller suppliers find hard to match. This is especially true when working with cost-conscious makers that can't afford production line downtime caused by late shipments.
The way we handle technical support makes the customer experience stand out. The in-house research and development lab offers custom formulation services 24 hours a day, 7 days a week. They help clients find the best side-chain lengths and functions for different types of cement or climate problems in their area. Support teams that speak English, Spanish, and Mandarin can help you in all three languages, so you can talk to them without any problems. This makes foreign hiring easier. Before committing to bulk orders, potential partners can test the product fully with their own equipment and local aggregates thanks to free sample programs. This method shortens the three- to six week decision cycle that most mid-sized PCE manufacturers have, turning inquiries into confirmed orders faster than competitors who sell generic products without application support.
Being responsible for the environment fits with market trends toward green building. EverStar Group wants to cut its carbon footprint by 30% by 2030, and it will help clients with LEED-certified projects and green building requirements. The EcoVadis Silver grade and Responsible Care® certification show that we are committed to using ethical production methods, which are becoming more and more important in developed markets when it comes to buying things. For companies that work with contractors who care about the environment or with government projects that need to be sustainable, working with a supplier that can show measurable ESG progress lowers regulatory risks and boosts the company's reputation.
Conclusion
Modern high-performance concrete technology relies on the Polycarboxylate Ether Monomer as a fundamental component. Because of the way its molecules are structured, it can reduce water, keep its shape, and make the concrete easier to work with in ways that other additive chemicals can't. Understanding important quality factors like unsaturation, hydroxyl value, and purity is important for successful procurement. Suppliers should also be judged on their store capacity, technical support, and compliance documents. Depending on the size of your production and how comfortable you are with risk, you can choose between buying strategies that focus on cost and those that focus on reliability. However, for mid-sized producers, factory-direct relationships always offer the best value. As the world's need for infrastructure grows, getting reliable monomer supplies from well-known companies is becoming more and more important for staying ahead in regional concrete markets.
FAQ
What differentiates TPEG from EPEG monomers in practical applications?
EPEG (Ethylene Glycol Monovinyl Polyethylene Glycol) has vinyl ether bonds that react at room temperature without any extra heat. This makes PCE production cheaper because it uses less energy. TPEG (Isopentenyl Alkenyl Polyethylene Glycol) needs high temperatures to work, but its side chains are a little longer, which helps it keep its shape in hot places. Manufacturers who want to save energy usually choose EPEG, while manufacturers who want to keep the workability of their products for a long time in tropical climates usually choose TPEG.
How should manufacturers store these monomers to prevent quality degradation?
Keep off-white to white flakes in sealed, moisture-proof containers in climate-controlled warehouses that stay between 15°C and 25°C. Stay out of strong sunlight, which can start polymerization that you don't want. If you store it for longer than three months, add stabilizers. Moisture contamination above 0.5% leads to caking and makes polymerization less effective, so controlling humidity is very important.
Can these monomers be used directly in concrete without processing?
Not at all. Polycarboxylate Ether Monomers need to be polymerized in water with acrylic acid and useful co-monomers in order to make active PCE superplasticizers. Adding something directly to concrete doesn't improve its performance. The synthesized polymer product is the only one that works well as an admixture.
Partner with a Trusted Polycarboxylate Ether Monomer Supplier
EverStar Group has been making things for 14 years and offers factory-direct prices that are 20–40% cheaper than those found through dealer outlets. With a minimum order quantity of only 5 tons, we can work with mid-sized PCE manufacturers who don't want to keep too much inventory on hand. We meet the strictest international quality standards because we are certified to REACH, FDA, ISO, and ASTM standards. Our expert team speaks many languages and can help you with free samples and formulations to speed up the process of making new products. You can email us at info@cneverstar.com to ask for product specifications, COA paperwork, or trial samples. You can look at our full selection of building chemical raw materials at cneverstar.com and learn how our dependable supply chain can help you stay ahead of the competition.
References
1. Ramachandran, V. S. (Ed.). (1995). Concrete Admixtures Handbook: Properties, Science, and Technology (2nd ed.). Noyes Publications.
2. Plank, J., & Hirsch, C. (2007). Impact of zeta potential of early cement hydration phases on superplasticizer adsorption. Cement and Concrete Research, 37(4), 537–542.
3. Uchikawa, H., Hanehara, S., & Sawaki, D. (1997). The role of steric repulsive force in the dispersion of cement particles in fresh paste prepared with organic admixture. Cement and Concrete Research, 27(1), 37–50.
4. Yoshioka, K., Tazawa, E., Kawai, K., & Enohata, T. (2002). Adsorption characteristics of superplasticizers on cement component minerals. Cement and Concrete Research, 32(10), 1507–1513.
5. ASTM International. (2019). ASTM C494/C494M-19: Standard Specification for Chemical Admixtures for Concrete. ASTM International.
6. Flatt, R. J., & Houst, Y. F. (2001). A simplified view on chemical effects perturbing the action of superplasticizers. Cement and Concrete Research, 31(8), 1169–1176.
Why Concrete Retarders Are Important in Modern Construction?
Concrete retarders, which act as specialized additives that slow down the hydration process of cement to increase workability time, have become indispensable in the modern building industry. As building projects get bigger and more complicated, these chemical solutions solve important problems like flash setting during hot weather pours, cold joint formation in mass concrete uses, and slump loss during long-distance transport. By giving builders reliable control over setting times, retarders help them get better finishing results while keeping the structure's integrity in a wide range of project situations.
Understanding Concrete Retarders and How They Work
Chemical Composition and Mechanisms
Set retardation is caused by certain functional groups in chemistry that stop the formation of calcium silicate hydrate crystals for a short time. Hydroxycarboxylic acids are often used in modern products, with sodium gluconate being one of the best examples. This white crystalline powder is ≥98.0% pure and works through a linear dose-response mechanism. It doesn't have the flash-set risks that come with options based on citric acid or sugar. It gives reliable delay windows of 2 to 7 hours at doses between 0.05% and 0.15% by cement weight. This lets procurement managers set exact handling times for complex pours.
Concrete retarders of the newer generation, unlike older lignosulfonate-based ones, keep the pH level in solution within a limited range of 6.2 to 7.8. This makes them compatible with polycarboxylate ether superplasticizers, which are often used in high-performance concrete mixes. The chloride level stays below 0.05%, which keeps the support steel from rusting. This is an important requirement for building projects that are meant to last for 50 years.
Physical Forms and Application Contexts
There are both liquid solutions and powder forms of retarding admixtures. Liquid forms are easier for automatic batching at ready-mix plants, while powder grades last longer and cost less to ship when buying from other countries. Which form to use relies on how much space you have for storage, the batching tools you have, and the humidity level where you live. When it comes to volumetric accuracy, ready-mix workers who work on multiple jobsites usually prefer liquids. On the other hand, precast makers often keep powders on hand for stocking flexibility.
Premium retarders can be used for more than just building. The same molecule works great in alkaline cleaning, bottle washing systems, and metal treatment processes at concentrations of 2% to 5%. This means that distributors can use the same SKU for construction, industrial cleaning, and even food-grade Applications that are in line with FCC, USP, and BP guidelines.
Benefits of Using Concrete Retarders in Modern Construction Projects
Enhanced Workability and Placement Flexibility
For large-scale structures, the concrete must be laid in a way that doesn't leave any weak spots. Concrete retarders keep the slump in place during long placement cycles. This lets teams work with complicated formwork designs without lowering the quality of the consolidation. Controlled hydration delay stops the concrete from stiffening too quickly between lifts, which could weaken the bond between lifts in tunnel lining projects or airport runway extensions where pours happen continuously for 8 to 12 hours.
According to ASTM C403, tests show that retarders that are properly dosed not only make the mix easier to work with for longer, but they also often make the 28-day compression strength 5% to 10% higher than control mixes. This increase in strength comes from more even crystal growth during the longer induction time, which makes the microstructure stronger. When purchasing engineers look at offers from suppliers, they should ask for performance data that shows strength ratios higher than 110% at normal test ages.
Hot Weather Concreting Solutions
When the temperature outside is above 35°C, the cement hydrates much faster, cutting the time it takes to set for the first time from 4 hours to less than 90 minutes. This speeding up of the heat causes cracks on the surface, lower final strength, and problems with finishing. These effects are canceled out by retarding admixtures, which make the dormant phase last longer. This lets evaporative cooling happen and the healing process work correctly. During the summer, retarders are often added to bridge deck fills in southwestern U.S. states to keep quality standards high.
The improved formulations' straight dosage response gives safety gaps that natural sugar-based retarders don't have. With natural sugar-based retarders, even a small overdose can cause setting delays that last for days or failure to set at all. This reliability cuts down on guessing in the field, which can cause project delays.
Environmental and Safety Advantages
Biodegradable retarders that meet OECD 301E standards and break down more than 90% in 28 days are used because people care about the environment. These eco-friendly choices work better than traditional chelators like EDTA at removing Fe³⁺ at alkaline pH levels above 11. This is important for coastal building where high-sulfate groundwater mixes with cementitious systems. Lower amounts of sulfate (0.05%) and heavy metals (Pb ≤10 ppm) are in line with standards for LEED-certified projects and city water quality rules.
Better safety features help the people who work with these products. When compared to acidic options, the near-neutral pH makes it less likely that the product will irritate the skin, and the fact that it meets REACH, FDA, HALAL, and KOSHER standards means that it will be accepted by regulators around the world.
How to Choose the Right Concrete Retarder for Your Project
Evaluating Project-Specific Requirements
The selection factors start with a study of the climate. In warm zones, projects may only need two to three-hour delays, which can be achieved with a 0.05% dose. In contrast, building in the desert needs five to seven-hour windows, which can only be achieved with a 0.12% to 0.15% dose. Procurement managers should ask for sample batch data that is specific to the site and is matched to the fineness of the cement, the amount of water in the gravel, and the ratios of water to cement.
It is necessary to test compatibility with current mixing packages. When concrete retarders are mixed with air-entraining agents or viscosity-changing additives, slump-loss tests and air-void spacing analysis must be done according to ASTM C231 to make sure that the goal air content of 5% to 7% stays stable over the longer placement time. Combinations that don't work well together can lead to quick slump collapse or too much bleeding, which can damage the quality of the surface finish.
Comparative Analysis of Supply Options
There are a lot of different formulas on the market, but sodium gluconate-based retarders are the best for buying in bulk. Distributors can easily keep track of their stock because they come in both food-grade and technical grade. This way, they can serve both concrete builders and industrial cleaning clients with approved products that meet FCC, USP, and BP standards. This variety in the market makes storing easier and improves the efficiency of cash flow.
To figure out the total cost of ownership, you have to look at more than just unit prices. Loss on drying specs (≤0.5%) and lowering substance content (≤0.5%) have a direct effect on the concentration of the active ingredient, which in turn changes the dosage rates that are used in real life. Products with more pollutants or wetness need higher doses to get the same delay effect, which cancels out any savings that might be seen. When you buy directly from a vertically integrated producer, you skip the middleman markups and save 20% to 40% on costs. Centralized quality control also makes sure that the products are the same from batch to batch.
Procurement Strategy Considerations
Sourcing choices are affected by things like minimum order amounts, shipping wait times, and the infrastructure for transport. When suppliers have plants close to big ports, freight costs are lower and restocking cycles are faster. Because 5-day trial services are available, buying teams can test performance with local aggregates before placing large orders. This lowers the risk of compatibility issues. When shipping goods across time zones, it's important to have technology help in multiple languages and customer service available 24 hours a day, seven days a week.
Strategic benefits come from long-term relationships with makers that offer OEM/ODM formulation creation. Custom formulas that are made to work best with local raw materials, like high-alkali fly ash or marine-dredged aggregates, give better performance than off-the-shelf goods. Access to proprietary mixing tools and on-site training speed up the training of workers, which cuts down on application mistakes that cause expensive project delays.
Application Best Practices and Troubleshooting for Concrete Retarders
Dosage Guidelines and Addition Timing
To dose correctly, you need testing equipment that is accurate to within 0.01%, especially when you are aiming for small retardation gaps. Adding concrete retarders during the first water charge makes sure they are evenly spread, but adding them later, in the middle of the mix, can sometimes make them work better. As part of quality control, ASTM C403 penetration resistance tests should be done every 30 minutes. This will allow real-time hydration curves to be created that prove the design assumptions.
Overdosing is still the most common mistake made in the field. It happens when workers try to fix sudden increases in temperature without recalculating the cement mass-based ratios. Recovery from a serious overdose may need controls on the cure environment and long-term tracking of strength according to ASTM C39. Because premium retarders have a linear reaction, there is some room for error. However, for large-scale operations, it is still best to keep detailed records of each batch and use automatic dispensing systems.
Storage and Shelf Life Management
Powder retarders stay stable for a year if they are kept in cases that are sealed and covered from UV light and kept at temperatures between 5°C and 30°C. To keep liquid concentrates from crystallizing, they need to be stored in a frost-free area. Purchasing teams that are in charge of multiple locations' stock should use first-in, first-out rotation rules and stability tests every three months to make sure of the purity of the products they sell. Each package needs to have a Certificate of Analysis (COA), Safety Data Sheets (SDS), and Technical Data Sheets (TDS). These documents make it possible for checks to follow the goods.
Even though sodium gluconate-based formulas are not very toxic, handling methods should include suggestions for personal protective equipment (PPE) for eye and respiratory safety and reduce the amount of dust that is created during powder transfer. Following the rules set by ISO 9001 quality management systems makes sure that providers keep written records of their control over the production, packing, and shipping processes.
Compatibility with Advanced Admixture Systems
These days, most concrete mixes have five or more chemical admixtures. Lab rheology tests are needed to see if retarders are compatible with polycarboxylate-based superplasticizers, shrinkage-reducing admixtures, and rust inhibitors. Mixtures that don't work well together can cause sudden increases in viscosity or delayed air release, which makes it harder to pump. If a supplier offers pre-blended admixture packages, there is no chance of mistakes when mixing in the field. However, custom formulas offer optimization options for specific uses like self-consolidating concrete or ultra-high-performance mixes.
Future Trends and Innovations in Concrete Retarder Technology
Sustainable Chemistry Advancements
Because the building industry wants to be carbon neutral, it is researching bio-based concrete retarders that come from farm waste. The new goods work just as well as the old ones, but they have 30% to 40% less carbon built into them. Manufacturers who put 5% of their annual income into research and development are making hybrid formulations that have both retardation and internal curing qualities. These formulations are designed to make single-component systems easier to work with and last longer.
Circular economy ideas affect how products are made, and molecules that break down easily, like sodium gluconate, are better for getting rid of waste at the end of their useful life than manmade chelators that don't break down. EcoVadis Silver-rated sellers show they care about the environment by having third parties check their energy use, water use, and trash management for factories that produce more than 50,000 tons of goods every year.
Digital Integration and Quality Assurance
IoT-enabled mixing systems now keep track of the rates at which retarder is added in real time and send that information to the cloud, where AI algorithms use weather forecasts and mix design factors to guess how the setting will behave. This digital integration makes quality control more accurate and gives buying managers performance data that help them negotiate with suppliers. Blockchain-based tracking systems make sure that Certifications like HALAL, KOSHER, and REACH are real. This stops fake goods from getting into global supply lines.
Predictive repair for storage bins and dispensing equipment cuts down on downtime as much as possible. With remote tracking, suppliers can offer proactive technical help and change dosage suggestions on the fly as project conditions change. These technological advances make ties between makers and contractors stronger by putting the focus on project success instead of just trading goods.
Strategic Supplier Partnerships
Forward-thinking buying strategies stress that suppliers can do more than just meet product requirements. Manufacturers with plants in the Southern, Eastern, and Northern regional groups protect themselves against supply problems and cut down on shipping costs. Diversified business structures that serve the markets for Food Additives and concrete show that they are financially stable and have a lot of technical knowledge. Getting certifications from SGS, Intertek, and the Responsible Care® program shows that you care about safety and the environment.
Contractors can become more skilled faster and learn from mistakes less often if they have access to application engineering resources like usage videos, product guides, and math tools. Free sample programs let you test them on the job site before making big promises, which lowers the risk of poor performance. World-class seller partnerships that support multi-year procurement deals have a lot of technical depth, good logistics, and quick responses to customer service requests.
Conclusion
It is impossible to say enough about how important concrete retarders are in modern buildings. These specialized chemicals solve important problems like placing in hot weather and managing the temperature of large amounts of concrete. Newer versions are better for the environment because they break down naturally and are less harmful. When making purchases, companies should look for suppliers that offer technical-grade sodium gluconate that has been tested and shown to meet ASTM C494 Type B standards. These suppliers should also have full certifications and quick technical support. As the need for infrastructure grows and rules about sustainability get stricter, builders can meet changing industry standards while keeping costs low by forming partnerships with makers that focus on new ideas.
FAQ
Can retarders reduce final concrete strength?
When used in the amounts suggested by the maker, concrete retarders usually make mixes stronger after 28 days by 5 to 10 percent compared to mixes that haven't been fixed. The longer hydration time lets crystals form more completely, which makes the microstructures thicker. Overdosing can slow down strength gain, which means that fixing and tracking must last longer according to ASTM C39 guidelines.
How do I calculate the correct dosage for my project?
Doses range from 0.05% to 0.15% by mass of cement, based on how long of a wait is wanted and the temperature of the area. It is still necessary to do site-specific test runs that are tuned to local materials. Actual retardation curves are set by penetration resistance tests according to ASTM C403. These may be different from general standards because of changes in the cement's alkali content and the amount of water in the aggregate.
Are eco-friendly retarders as effective as traditional options?
In many situations, biodegradable retarders based on sodium gluconate work better than regular ones. Their linear dose-response gets rid of flash-set risks and achieves >90% decline within 28 days, which is what OECD 301E standards say should happen. They work especially well in high-sulfate seaside settings because they are better at chelating iron at alkaline pH levels.
Partner with EverStar Group for Reliable Concrete Retarder Supply
EverStar Group has factory-direct concrete retarders that meet the standards for ASTM C494, EN 934, and REACH compliance and are ready to help you with your building projects. Our ISO 9001, HALAL, and KOSHER standards back up our production capacity of more than 50,000 tons per year, which we use to serve Fortune 500 clients in 50 countries. Standard goods are sent out within three days, and custom formulations are sent out within five to seven days. We offer expert help in multiple languages 24 hours a day, seven days a week. Request free samples today to see how well they work with the rocks in your area. Our team can help you improve your concrete operations with mixing tools, usage videos, and on-site training. Get in touch with our concrete retarder sources at info@cneverstar.com to talk about your buying needs and find out how direct manufacturer partnerships can save you 20% to 40% on costs.
References
1. American Society for Testing and Materials (2021). ASTM C494: Standard Specification for Chemical Admixtures for Concrete. West Conshohocken: ASTM International.
2. Ramachandran, V.S. & Beaudoin, J.J. (2019). Handbook of Analytical Techniques in Concrete Science and Technology: Principles, Techniques, and Applications. Norwich: William Andrew Publishing.
3. Mehta, P.K. & Monteiro, P.J.M. (2020). Concrete: Microstructure, Properties, and Materials (Fifth Edition). New York: McGraw-Hill Education.
4. Mindess, S., Young, J.F. & Darwin, D. (2018). Concrete (Second Edition). Upper Saddle River: Pearson Education.
5. Neville, A.M. (2022). Properties of Concrete (Sixth Edition). London: Pearson Education Limited.
6. Kosmatka, S.H., Wilson, M.L. & Kerkhoff, B. (2020). Design and Control of Concrete Mixtures (Sixteenth Edition). Skokie: Portland Cement Association.
- 1
- 2
- 3